OEM Custom Machined Steel Components Manufacturer for Sale
Selecting a Custom Machined Steel Components OEM Guide partner requires prioritizing process control over initial quotes to prevent costly site failures. Learn to evaluate clamping strategies, verify...
OEM Custom Machined Steel Components Manufacturer for Sale
Lowest unit price often leads to the highest total project cost.
Selecting a partner for Custom Machined Steel Components OEM Guide requires prioritizing process control and drawing fidelity over initial quotes to prevent costly site installation failures. The critical differentiator is not the machine brand, but the supplier’s ability to maintain tolerance stability through proper clamping and verification protocols before shipment.
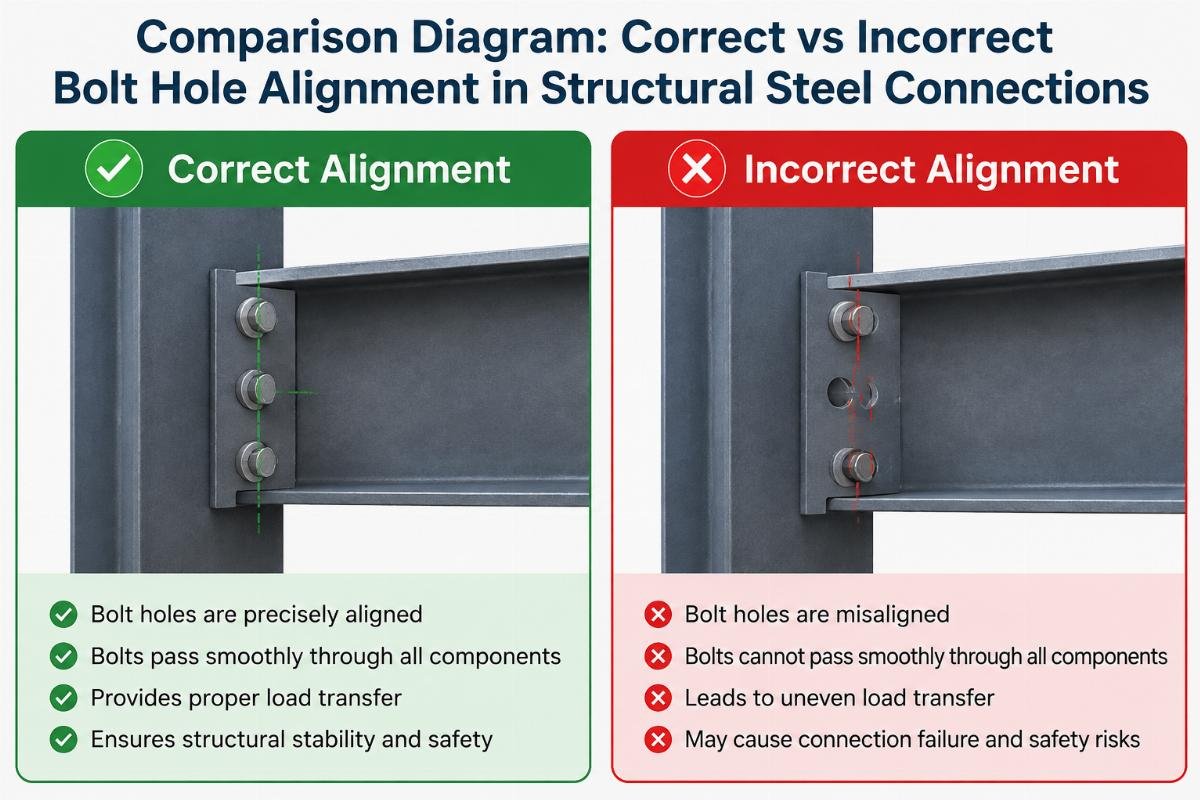
I still remember the humidity in Riyadh during a municipal parking structure project. A batch of embedded machined connection plates arrived on site with bolt hole deviations that looked acceptable to the naked eye but failed under engineering scrutiny. The drawings specified a tight positional tolerance, yet the drilled holes were off by nearly two millimeters. The steel beams simply would not align. The contractor demanded immediate replacement, and the air freight costs for the emergency reshoot exceeded the original savings from choosing the cheaper vendor by a significant margin. That incident shifted my focus entirely. Now, when I evaluate a facility for Custom Machined Steel Components OEM Guide, I do not start with the price list. I walk into the workshop to observe how they fixture thin-walled sections and how they validate first-article inspections. [NEED_CITE: impact of tolerance accumulation on structural assembly]
This approach separates vendors who merely cut metal from those who engineer solutions. The following analysis breaks down the technical realities of sourcing these critical parts.
Why Do Standard Machined Parts Fail on Site?
Tolerance accumulation and drawing interpretation errors are the primary causes of field rejection.
Many buyers assume that if a part looks correct individually, it will fit into the larger structure. This is a dangerous misconception in structural steel fabrication. When multiple machined interfaces connect—such as beam-to-column joints or expansion joint plates—minor deviations in each component compound rapidly. A half-millimeter error in one plate might be manageable, but when ten such plates align across a bridge span, the cumulative deviation can render the entire assembly unbuildable. [NEED_CITE: principles of geometric dimensioning and tolerancing in structural steel]
In industrial warehouse projects, I have seen weld prep misalignments caused by poor clamping strategies. If a supplier does not account for thermal distortion or mechanical stress during the machining process, the final dimensions will drift once the part is released from the vise. This is particularly common in large-scale Custom Machined Steel Components OEM Guide orders where batch consistency is challenging.
Failure Mode
Root Cause
Field Consequence
Bolt Hole Misalignment
Inaccurate CNC positioning or drill wander
Inability to insert high-strength bolts; requires reaming or rejection
Surface Flatness Deviation
Improper clamping of thin plates
Gaps in bearing surfaces; uneven load distribution
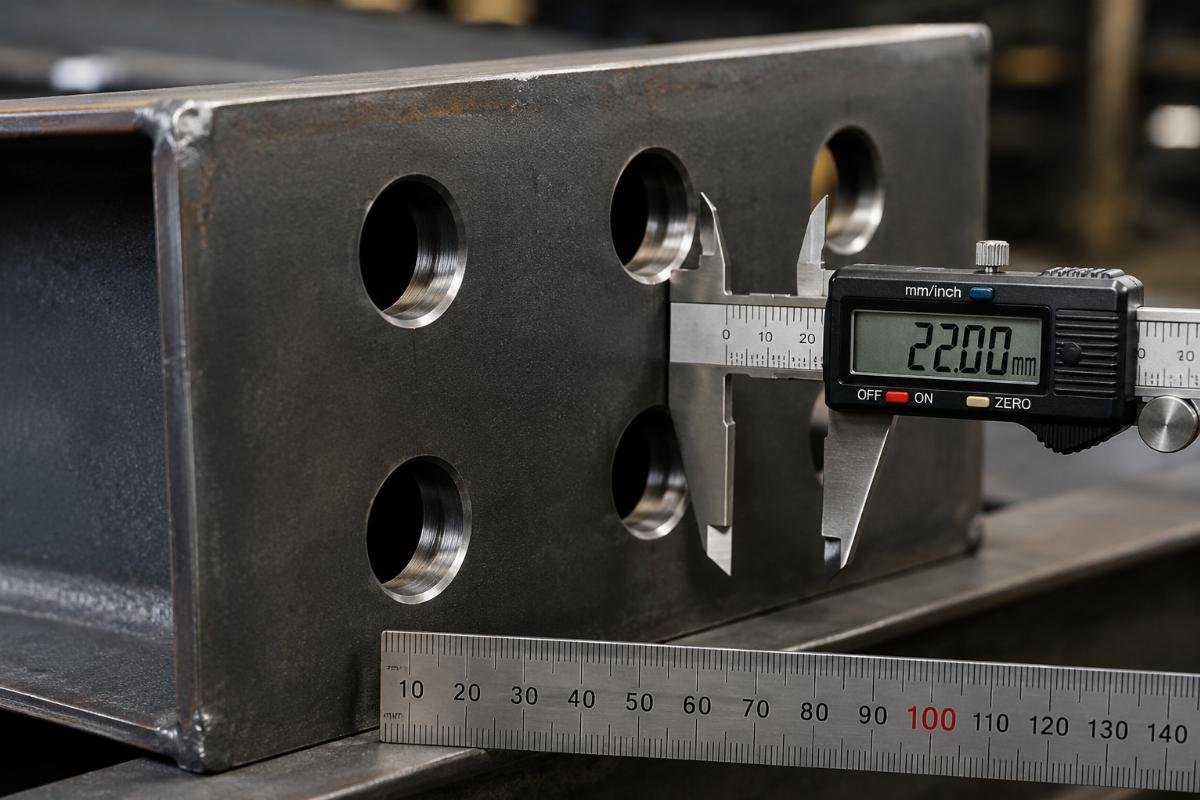
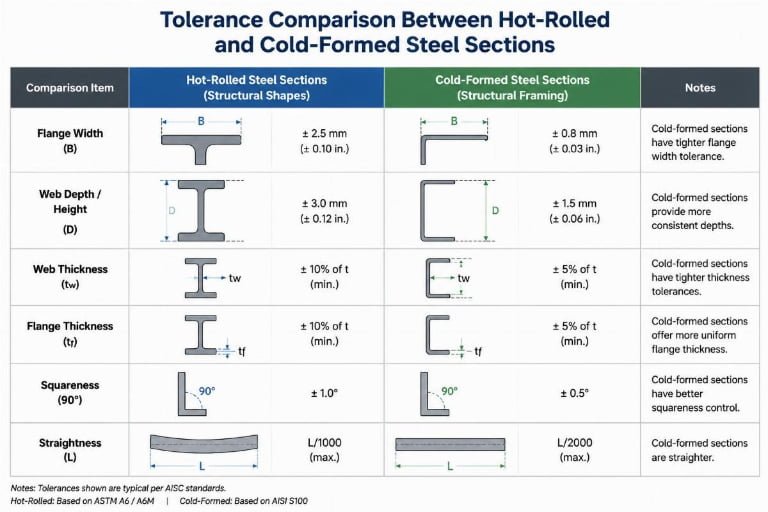
A Middle East fabricator once reported that nearly all their rework costs stemmed from these interface issues rather than material defects. By focusing on the critical tolerance zones for structural interfaces, buyers can avoid these pitfalls. The key is to demand detailed inspection reports that verify hole position and flatness against international standards like EN10219. [NEED_CITE: EN10219 tolerance requirements for cold-formed structural hollow sections]
How to Evaluate a Supplier’s Process Control?
Assess clamping methods, in-house lab capabilities, and first-article inspection rigor.
CNC machines are only as precise as the setup holding the workpiece. A common mistake is assuming that high-end equipment guarantees precision. In reality, improper fixturing leads to deformation regardless of the machine’s quality. For Custom Machined Steel Components OEM Guide sourcing, I look for suppliers who use specialized fixtures for non-standard shapes rather than relying on generic vises.
During a visit to a production facility in Jinan, I observed their approach to thin-walled rectangular hollow sections. Instead of standard clamps that could crush the profile, they used custom mandrels and soft-jaw fixtures to maintain dimensional stability during milling. This attention to detail is what prevents the “ovalization” of square tubes during machining. [NEED_CITE: best practices for fixturing thin-walled steel components]
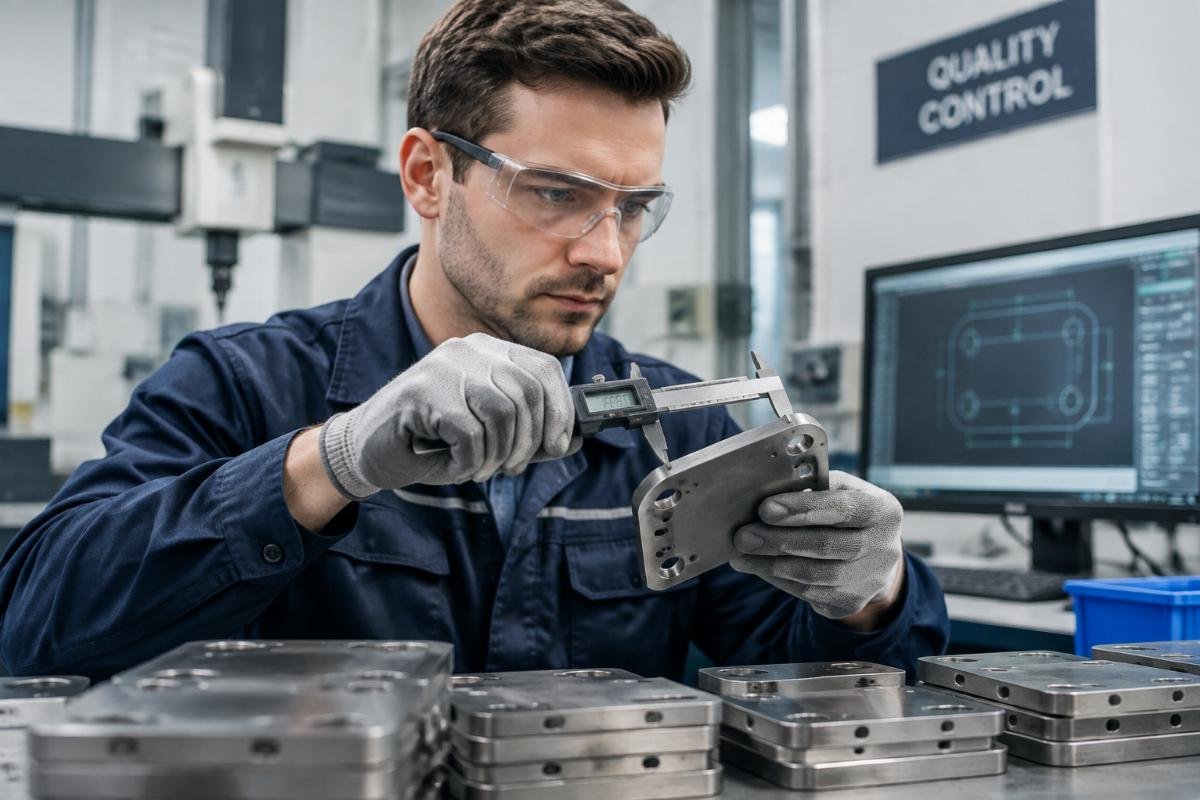
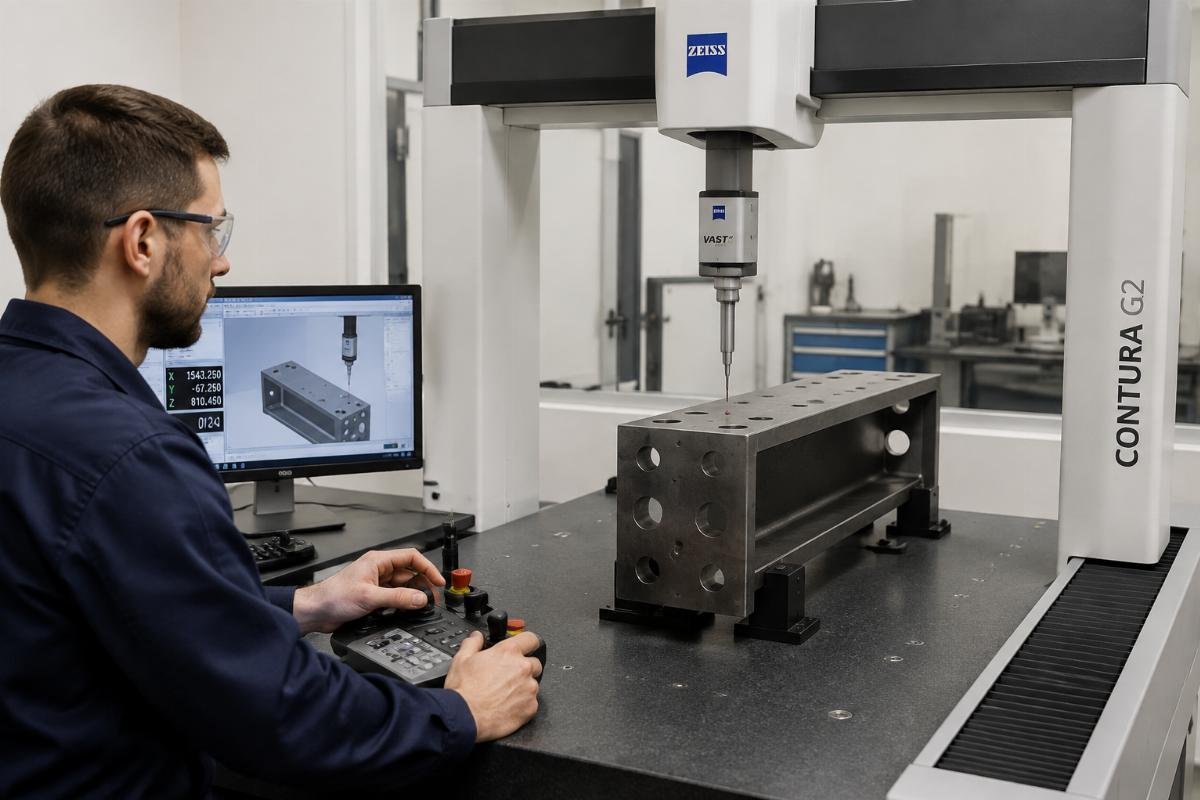
Verification protocols also vary widely. Some suppliers rely solely on manual caliper checks, which are prone to human error. Others invest in Coordinate Measuring Machines (CMM) to generate comprehensive digital reports. A CMM report provides verifiable data on every critical dimension, offering a level of assurance that manual checks cannot match.
Verification Method
Accuracy Level
Data Traceability
Manual Caliper/Micrometer
Operator-dependent
Low; paper-based logs
Optical Comparator
Moderate
Medium; image capture
CMM (Coordinate Measuring Machine)
High; micron-level
High; digital 3D model comparison
The manufacturer’s production facilities should demonstrate an integrated workflow where quality control is not an afterthought but a parallel process. In-house laboratories allow for immediate feedback loops. If a first-article inspection fails, the machine parameters can be adjusted before the full batch runs. This capability is essential for maintaining consistency in large orders of Custom Machined Steel Components OEM Guide.
What Tolerances Matter Most for Structural Steel?
Differentiate between general machining tolerances and critical fit-up dimensions.
Not all dimensions on a drawing carry equal weight. General surface finishes may have loose tolerances, but interface points—where steel meets steel—require strict adherence. For structural applications, the position of bolt holes and the flatness of bearing surfaces are paramount. A deviation in hole position can prevent assembly, while poor flatness can compromise load transfer. [NEED_CITE: ISO 2768 general tolerances for linear and angular dimensions]
In bridge expansion joint plates, surface treatment inconsistency can affect fit. Shot blasting profiles must be uniform to ensure that protective coatings adhere properly without altering the dimensional stability of the part. If the blasting is too aggressive, it can remove material from critical edges, pushing the part out of tolerance.
Critical Feature
Typical Tolerance Requirement
Impact of Deviation
Bolt Hole Position
±0.5 mm to ±1.0 mm
Assembly failure; need for rework
Bearing Surface Flatness
≤ 0.5 mm over 1 meter
Uneven load distribution; potential buckling
Weld Bevel Angle
±2.5 degrees
Poor weld quality; structural integrity risk
Understanding these distinctions helps buyers communicate effectively with suppliers. Instead of asking for “high precision,” specify the critical zones that require tight control. This targeted approach ensures that the manufacturer focuses resources where they matter most, optimizing both cost and quality for Custom Machined Steel Components OEM Guide projects.
Which Certifications Ensure Consistent Quality?
Role of EN10210/EN10219 and mill test certificates in verifying material and process integrity.
Certifications are not just paperwork; they are evidence of a systematic approach to quality. For European and international projects, compliance with EN10219 for cold-formed welded structural hollow sections and EN10210 for hot-finished sections is non-negotiable. These standards dictate not only material properties but also dimensional tolerances and testing frequencies. [NEED_CITE: differences between EN10219 and EN10210 standards]
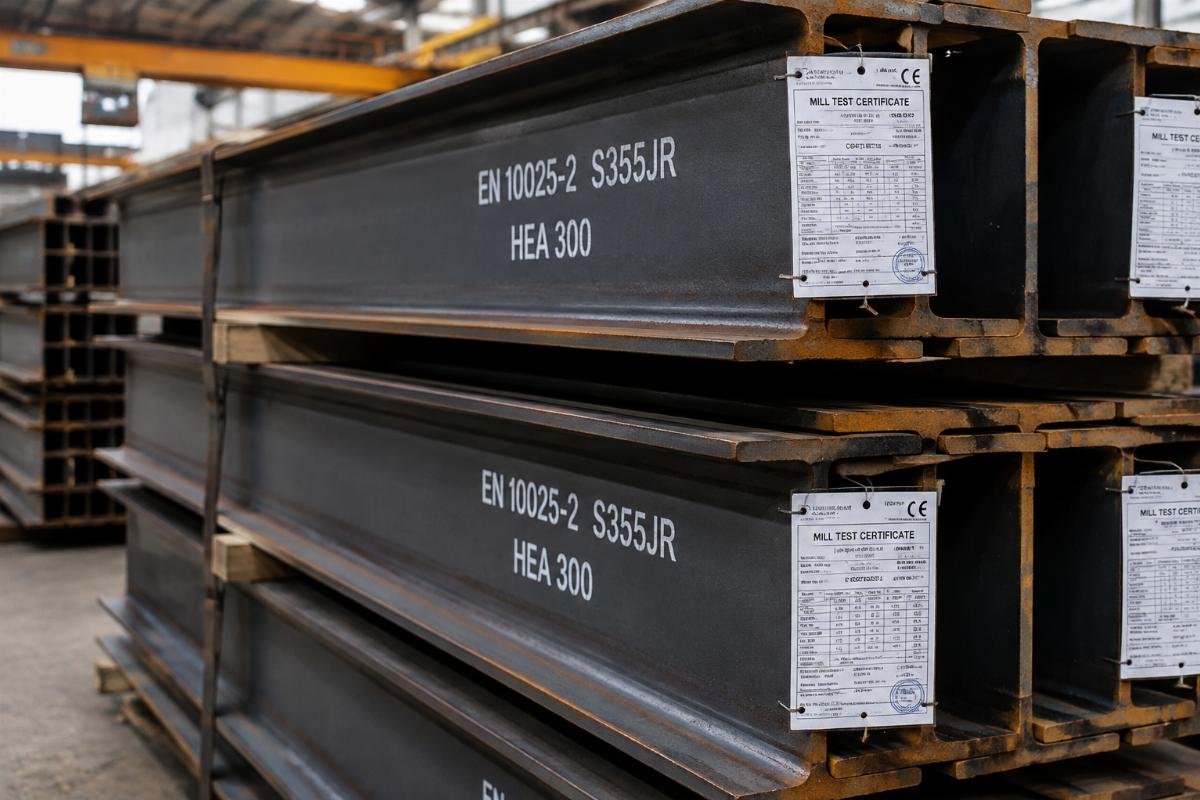
Mill Test Certificates (MTCs) provide traceability back to the raw material source. They confirm the chemical composition and mechanical properties of the steel, ensuring it meets the required grade such as S355JR or Q345B. Without valid MTCs, there is no guarantee that the steel will perform under load, regardless of how precisely it was machined.
Additionally, third-party certifications like ISO 9001 indicate that the supplier has a documented quality management system. This system ensures that processes are repeatable and that deviations are recorded and addressed. For buyers seeking Custom Machined Steel Components OEM Guide, verifying these credentials is a crucial step in risk mitigation.
Certification/Document
Purpose
Verification Value
EN10219 / EN10219
Structural product standard
Ensures dimensional and material compliance
Mill Test Certificate (MTC)
Material traceability
Confirms grade and mechanical properties
ISO 9001
Quality management system
Validates process consistency and documentation
A supplier’s ability to provide these documents promptly and accurately reflects their operational maturity. It signals that they understand the regulatory landscape and are prepared to support international construction projects with the necessary documentation.
Conclusion
Precision in machining is defined by process control, not just machine capability.
Sourcing Custom Machined Steel Components OEM Guide partners requires a shift from price-focused evaluation to technical due diligence. By prioritizing tolerance management, robust clamping strategies, and verified certifications, buyers can prevent expensive site failures. The goal is to ensure that every component fits perfectly the first time, safeguarding the project timeline and budget.
Editor covering global sourcing, supplier verification, and industrial product knowledge. Content is compiled from manufacturer specifications, industry standards, and hands-on experience with international B2B buyers. Every article is fact-checked before publishing to help procurement professionals make informed decisions.

Discussion
0 Comments