
Description
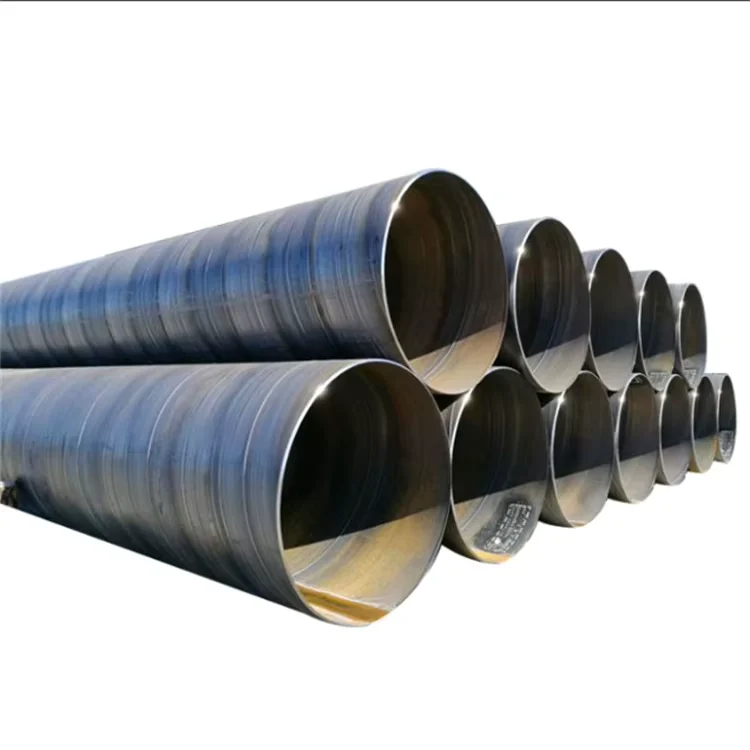
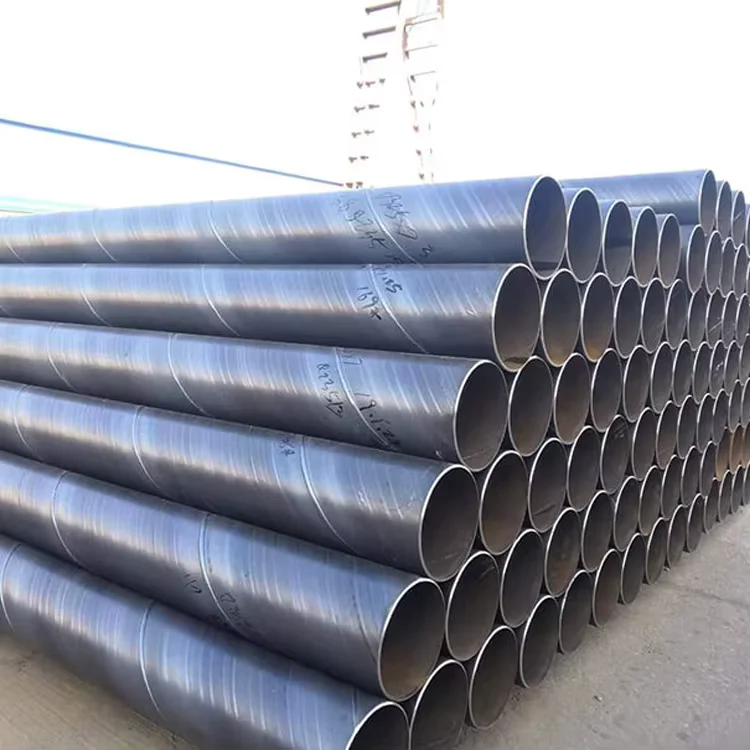
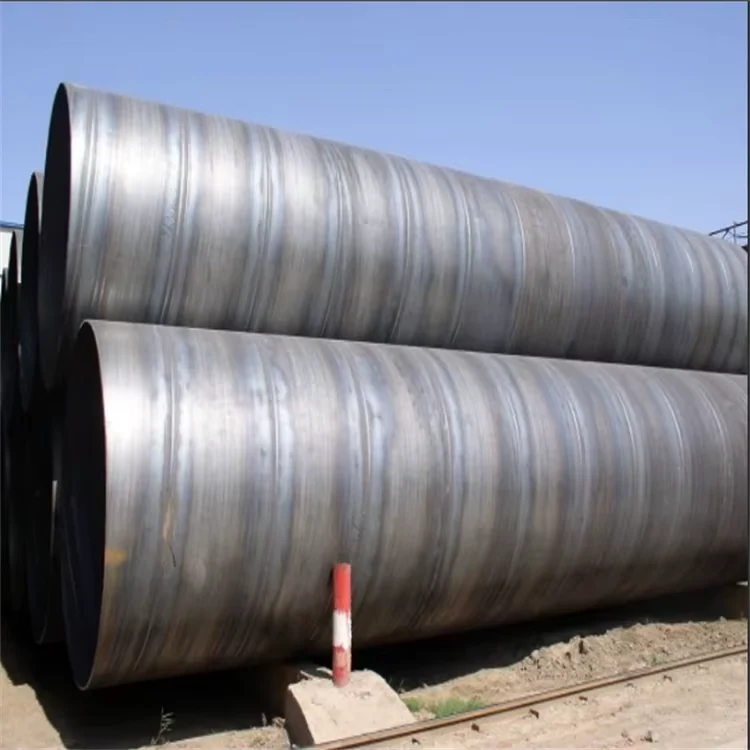
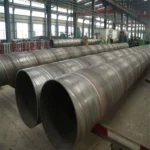
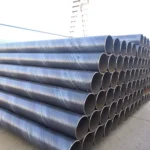
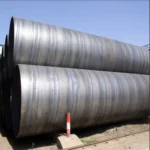
Factory-Direct SSAW Spiral Welded Steel Pipe Supply — Bulk SSAW spiral welded steel pipe supplier delivering API 5L and ASTM grades with original mill test certificates and optimized container loading for large-diameter cargo.
Technical Specifications
| Parameter | Value |
|---|---|
| Designation | Q345R GR70 SSAW Welded Carbon Steel Pipe |
| Product Type | SSAW Welded Steel Pipe |
| Steel Grade | Q235, Q345, Q345B, Q345C, Q345A, Q195, Q215, 10#, 20#, 45#, 16Mn, ASTM A53A, A53B, A106B, API 5L (Gr.B, X42, X46, X52, X60, X65, X70, X80, X100), ST37, ST37-2, DIN 1629 ST35, ST45, DIN 17175 ST35.8, 19Mn5, T1, T2, T5, T9, T11, T12, T22, T91, T92, P1, P2, P5, P9, P11, P12, P22, P91, P92, 15CrMo, Cr5Mo, 10CrMo910, 12CrMo, 13CrMo44, 30CrMo, A333 GR.1, GR.3, GR.6, GR.7 |
| Standard | ASTM A53, ASTM A106, API 5L, BS, DIN, GB, JIS, EN |
| Section Shape | Round |
| Size Range | OD 21.3–1420 mm |
| Wall Thickness | 2–300 mm |
| Length | 5.8 m / 6 m / 11.8 m / 12 m |
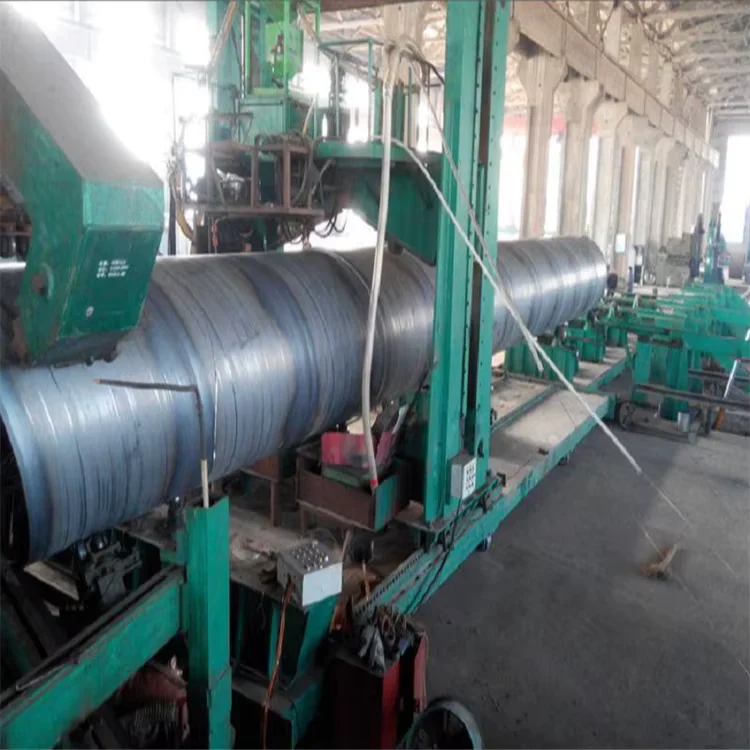
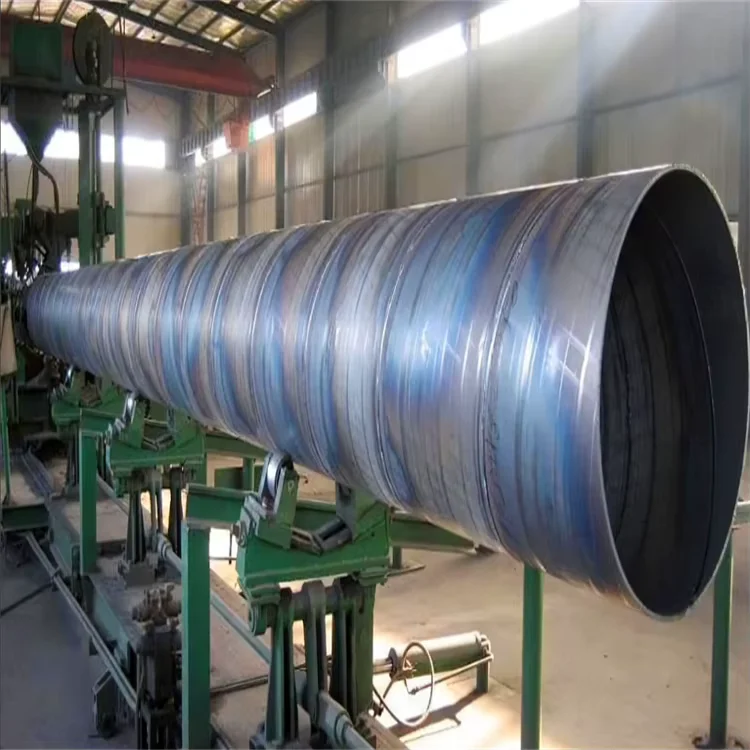
| Technique | SSAW (Spiral Submerged Arc Welded) / Hot Rolled |
| Surface Treatment | 3PE / Epoxy Coated / Black / Oiled / Non-oiled |
| Tolerance | ±1% |
| Ends | Plain / Beveled (with Plastic Pipe Cap end protector) |
| Application | Fluid transportation (oil, gas, water) / Structure / Construction / Machinery parts / Automobile and tractor stress parts / Boiler / Chemical fertilizer pipe / Drill pipe / Hydraulic pipe |
| MOQ | 1 Ton (sample order accepted) |
| Origin | Shandong, China |
Application Suitability
| Industry | Typical Applications |
|---|---|
| Oil & Gas Transmission | Long-distance crude oil and natural gas pipelines, gathering lines, 3PE coated API 5L X42–X80 trunk lines |
| Municipal Water Infrastructure | Raw water intake and distribution mains, sewage force mains, large-diameter water transfer projects |
| Structural & Construction | Bridge piers, stadium roof trusses, industrial plant columns, piling support structures |
| Power & Energy | Boiler feed water lines, cooling water circuits, coal ash slurry transport in thermal power plants |
| Chemical & Fertilizer | Process piping for fertilizer plants, corrosive fluid conveyance with epoxy lining |
Where Coating Adhesion Failure Turns a Pipeline Order into a Forty-Day Delay
Surface treatment integrity on large-diameter SSAW pipe determines whether the cargo passes site inspection or gets rejected at the trench.
I once watched a 3,000-ton shipment of 3PE coated SSAW spiral pipe arrive at Manila port for a hydropower project. The coating剥离强度 came in at less than half the specified minimum — the 3PE layer was peeling before the pipes even reached the trench. The supervising engineer rejected the entire batch. Forty days of rework, missed deadlines, and a supplier who blamed the shipping humidity. The root cause traced back to inadequate surface pretreatment and poor temperature control during the polyethylene extrusion wrap. On spiral seam welds, the geometry makes uniform coating adhesion harder than on straight-seam pipe, and not every factory runs the process window tightly enough. [NEED_CITE: 3PE coating adhesion requirements per DIN 30670 / ISO 21809]
Matching Large-Diameter SSAW Pipe to High-Pressure and Structural Applications
This SSAW spiral welded steel pipe covers OD up to 1420 mm and wall thickness up to 300 mm, placing it squarely in the range required for high-pressure oil and gas trunk lines and heavy structural columns. The spiral submerged arc welding process produces a continuous helical seam that distributes stress more evenly across the pipe body compared to longitudinal seam alternatives on larger diameters. For corrosive service environments — offshore platforms, chemical fertilizer plants, buried municipal water mains — the 3PE and epoxy coating options provide layered corrosion protection that meets DIN 30670 and ISO 21809 application standards. API 5L grades from Gr.B through X100 cover the full pressure spectrum from low-pressure water distribution to high-strength sour gas transmission, while Q345B and ASTM A53 grades serve structural framing where weldability and formability matter more than ultimate tensile strength.
Engineering Compliance and Certification Requirements for Pipeline and Structural Projects
Pipeline projects governed by ASME B31.4 or B31.8 require documented material traceability back to the heat number, and the API 5L specification mandates specific chemical composition limits and mechanical property testing for each grade designation. Structural applications under EN 1993 or AISC demand that the steel grade conforms to the declared standard with verified yield and tensile values. For EU-bound shipments, CE certification under EN 10210 or EN 10219 is often a customs clearance prerequisite — missing paperwork means the cargo sits at the port while the project waits. [NEED_CITE: CE marking requirements for structural hollow sections under EN 10210] The ±1% tolerance on OD and wall thickness ensures that field cutting, beveling, and fit-up for girth welding proceed without unexpected dimensional deviations. Fixed lengths of 5.8 m, 6 m, 11.8 m, and 12 m align with standard container and flat-rack configurations, reducing on-site cutting waste.
Steel Grade Selection and SSAW Process Fundamentals
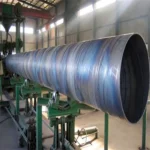
The API 5L grade system designates minimum yield strength in psi units — X42 indicates 42,000 psi, X70 indicates 70,000 psi — and higher grades allow thinner walls for the same design pressure, reducing material weight and transport cost per kilometer of pipeline. The Q-series grades (Q195 through Q345) follow the Chinese GB standard system where the number denotes minimum yield strength in MPa, making Q345B roughly equivalent to S355 in the EN system and ASTM A572 Gr.50 in the US system. SSAW spiral submerged arc welding forms the pipe from a continuously fed steel coil, spiraling it at a controlled angle and welding both the inner and outer seams simultaneously under a flux blanket. This process excels at producing large diameters — up to 1420 mm — from relatively narrow coil widths, which keeps raw material cost lower than plate-based alternatives for the same OD. [NEED_CITE: SSAW vs LSAW manufacturing process comparison for large-diameter pipe] The 3PE coating system applies a fusion-bonded epoxy primer, a copolymer adhesive interlayer, and an extruded polyethylene outer jacket in a single continuous line — each layer must bond metallurgically to the previous one, and the spiral weld seam geometry requires precise torch and die alignment to avoid thin spots at the weld crown.
Hidden Costs of Procuring SSAW Pipe Without Verified Documentation
Ordering SSAW pipe based on price alone, without requiring original mill test certificates tied to specific heat numbers, creates a chain of risk that surfaces at the worst possible moment — site inspection. Material that does not match the declared grade will fail mechanical testing at the project lab, triggering batch rejection and forcing emergency re-procurement at spot market premiums. Missing CE or ISO certificates block customs clearance in regulated markets, generating demurrage charges that can exceed the pipe cost itself. Wall thickness that falls below the declared tolerance — a practice some mills use to ship heavier theoretical weight at lower actual weight — compromises pressure ratings and structural load capacity, creating safety liability that no amount of cost savings can offset. [NEED_CITE: consequences of non-conforming steel materials in pipeline construction]
Why Project Buyers Source SSAW Spiral Welded Steel Pipe from Xin Jiyuan
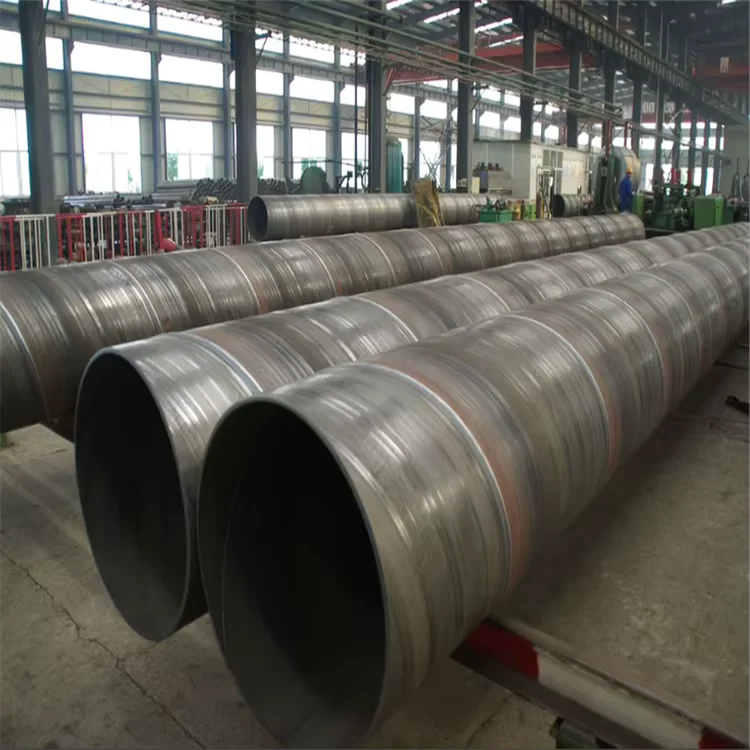
Xin Jiyuan operates three SSAW production lines running simultaneously, delivering monthly capacity exceeding 20,000 tons of spiral welded pipe across the full OD and wall thickness range. Every shipment leaves the factory with original mill test certificates documenting chemical composition and mechanical properties per the declared API 5L, ASTM, or GB grade — no generic certificates copied across batches. The in-house laboratory holds CNAS accreditation for tensile, impact, and chemical analysis, and third-party SGS or BV inspection can be arranged before shipment for buyers who require independent verification. With over 2,800 specifications in ready stock covering standard OD and wall thickness combinations, urgent orders and split shipments can be fulfilled without waiting for production slots. The professional export team handles container loading optimization for heavy large-diameter pipe, ensuring weight distribution meets port crane limits and maximizing payload per shipment. ISO 9001:2015, Lloyd’s CE (EN 10210/10219), and FPC certifications are maintained and available for project compliance documentation.
Documentation & Compliance
- Mill test certificate documenting Q345B or API 5L X52 chemical composition and yield strength per GB/T 9711 or API 5L, tied to specific heat number
- CE certificate per EN 10210 / EN 10219 for structural hollow sections shipped to EU member states
- ISO 9001:2015 quality management system certificate covering the full SSAW production process
- SGS or BV third-party inspection report available upon request for independent verification of dimensions, coating thickness, and mechanical properties
- Material traceability documentation linking each pipe to its heat number, production date, and test batch
- Full customs document package including packing list, bill of lading, and certificate of origin for destination port clearance
Packaging, Loading & Delivery
- SSAW spiral welded pipes bundled with steel strips in seaworthy packaging, with plastic end caps protecting beveled ends from impact damage during transit
- 3PE coated pipes handled with nylon sling separators and edge protectors to preserve the polyethylene coating from abrasion during loading and ocean freight
- Container loading optimized for 5.8 m and 6 m lengths in 20ft and 40ft containers, with 11.8 m and 12 m lengths shipped on flat racks or breakbulk depending on destination port crane capacity
- Heat number and steel grade stenciled on each pipe end for on-site identification and traceability verification during installation
- FOB, CIF, and DDP shipping terms available, with professional logistics coordination from Jinan inland port to destination ports across Southeast Asia, Middle East, Africa, and South America
Submit Your Specifications for a Detailed SSAW Pipe Quotation
Provide your required OD, wall thickness, steel grade, surface treatment, quantity, and destination port — the technical team responds within 12 hours with competitive bulk pricing, available stock confirmation, and a delivery schedule. Non-standard dimensions and custom coating specifications can be reviewed for feasibility and lead time.
Get Your SSAW Spiral Welded Steel Pipe Quote with Mill Test Certificates
Send your specification sheet to admin@sdxinjiyuan.com or contact via WhatsApp at +86 188 5315 7756 to receive pricing, available stock status, and certification documentation for your next pipeline or structural project.
Frequently Asked Questions
Q: How do API 5L, ASTM A53/A106, and GB steel grades compare when selecting SSAW pipe for a project?
A: API 5L grades (Gr.B through X100) are designed specifically for pipeline transmission and specify minimum yield strength in psi units. ASTM A53 covers general pressure and mechanical applications in Grades A and B, while ASTM A106 is intended for high-temperature service. Chinese GB grades like Q235 and Q345B specify minimum yield strength in MPa and are widely used in domestic and international structural and pipeline projects. Xin Jiyuan supplies all three standard systems and can provide grade cross-reference guidance based on your project specification.
Q: What documentation is provided with each shipment, and can third-party inspection be arranged?
A: Every batch ships with original mill test certificates documenting chemical composition and mechanical properties per the declared standard, with full traceability to the heat number. ISO 9001:2015 and CE (EN 10210/10219) certificates are available for project compliance. Third-party inspection by SGS or BV can be arranged before shipment for independent verification of dimensions, coating thickness, and mechanical test results.
Q: When should I specify 3PE coating versus epoxy coating versus black or oiled finish for SSAW pipe?
A: 3PE coating (fusion-bonded epoxy primer, copolymer adhesive, and extruded polyethylene outer layer) is the standard choice for buried or submerged oil, gas, and water pipelines where long-term corrosion protection is critical. Epoxy coating alone suits internal linings or moderate external corrosion environments. Black or oiled finish is appropriate for above-ground structural applications, temporary storage, or projects where field coating will be applied after installation.
Q: Can non-standard outer diameter, wall thickness, or length be produced, and what is the minimum order quantity?
A: Custom OD, wall thickness, and length specifications can be produced on the SSAW lines, with typical lead times of 15–25 days depending on the specification and order volume. The minimum order quantity is 1 ton, and sample orders are accepted for quality verification before bulk procurement.
Q: How is container loading optimized for large-diameter SSAW pipe, and what shipping terms are available?
A: The export team develops container loading plans that maximize payload while ensuring weight distribution meets port handling limits. Smaller diameter pipes in 5.8 m and 6 m lengths are loaded in standard 20ft and 40ft containers, while 11.8 m and 12 m lengths are shipped on flat racks or breakbulk vessels. FOB, CIF, and DDP shipping terms are available, with professional documentation and customs clearance support for destinations across Southeast Asia, Middle East, Africa, and South America.