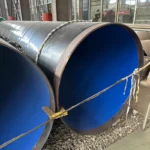
Description
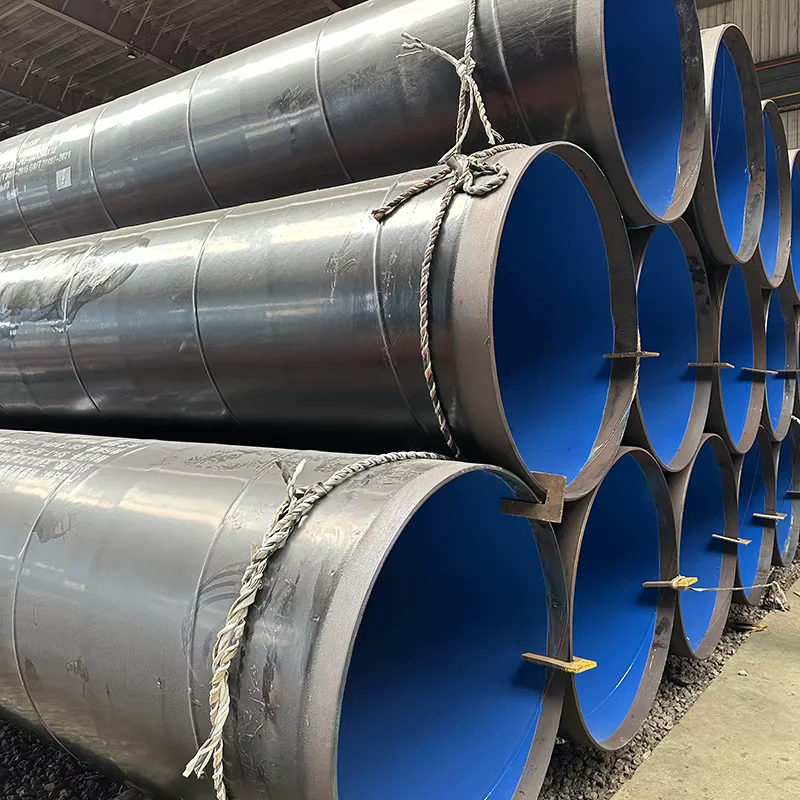
Factory-Direct SSAW Spiral Welded Steel Pipe Supply — Every Q235B pipe ships with original mill test certificates and API 5L traceability, priced directly from our Jinan production lines with no trading markup.
Technical Specifications
| Parameter | Value |
|---|---|
| Designation | Q235B SSAW Spiral Welded Steel Pipe |
| Product Type | SSAW Spiral Welded Steel Pipe |
| Steel Grade | Q195, Q235B, Q345B, A53, A106, 08F, 1.0033 |
| Standard | API 5L, API 5CT, SY/T5037, SY/T5040, GB/T9711.1, GB/T9711.2, ASTM A53, ASTM A106 |
| Section Shape | Round |
| Size Range | OD 219.1–2200 mm |
| Wall Thickness | 3–30 mm |
| Length | 5.8–11.8 m (or custom) |
| Technique | Submerged Arc Welding (SAW) / Spiral Welded |
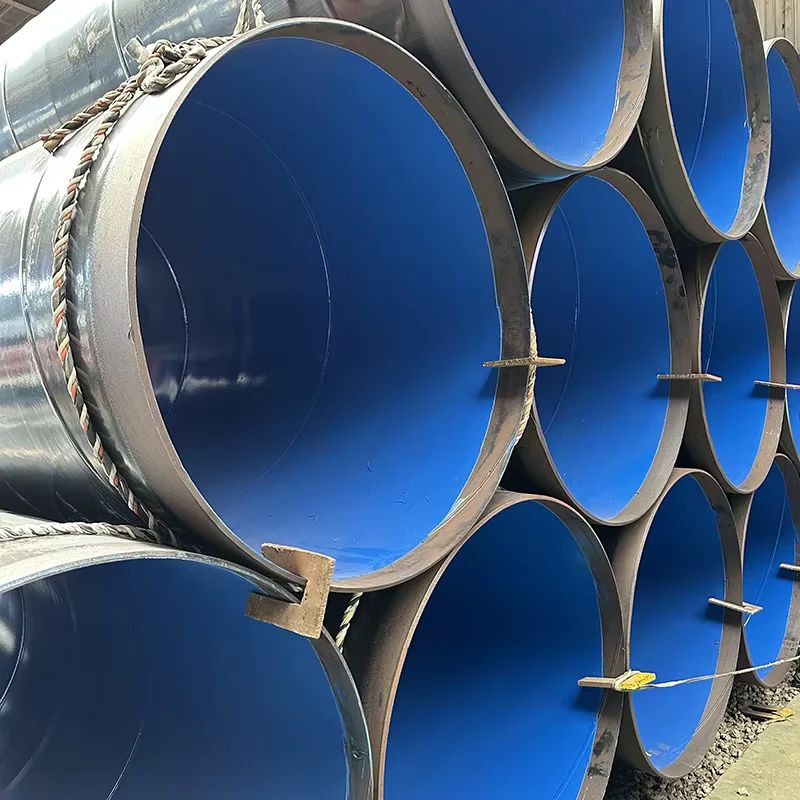
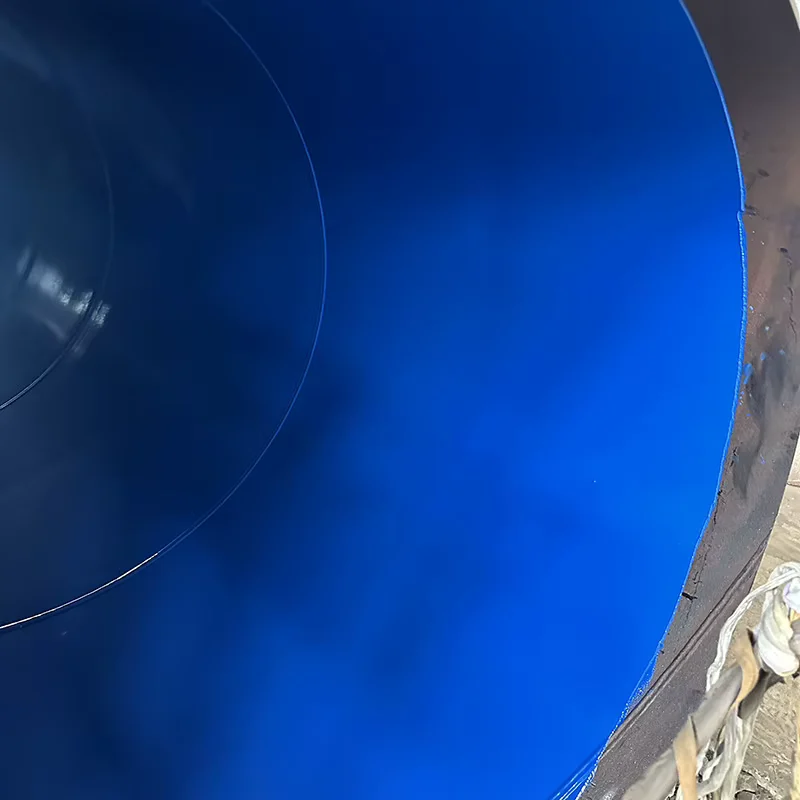
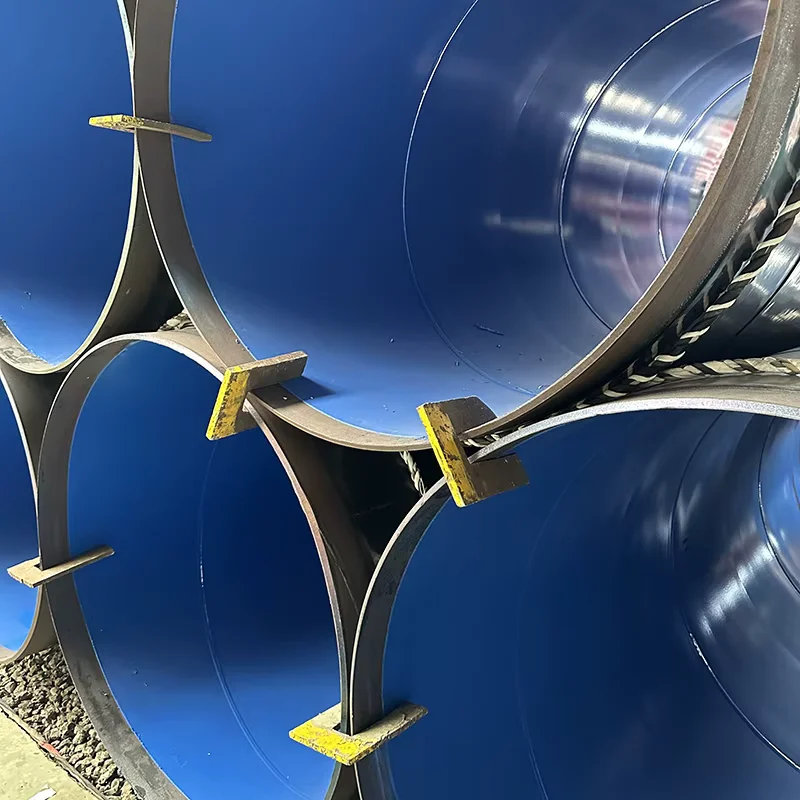
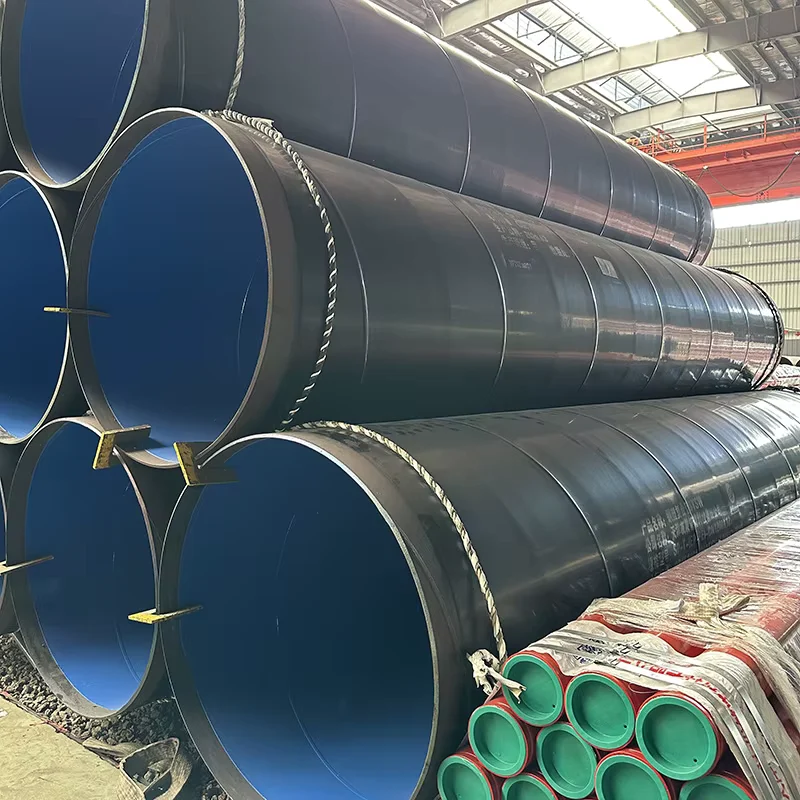
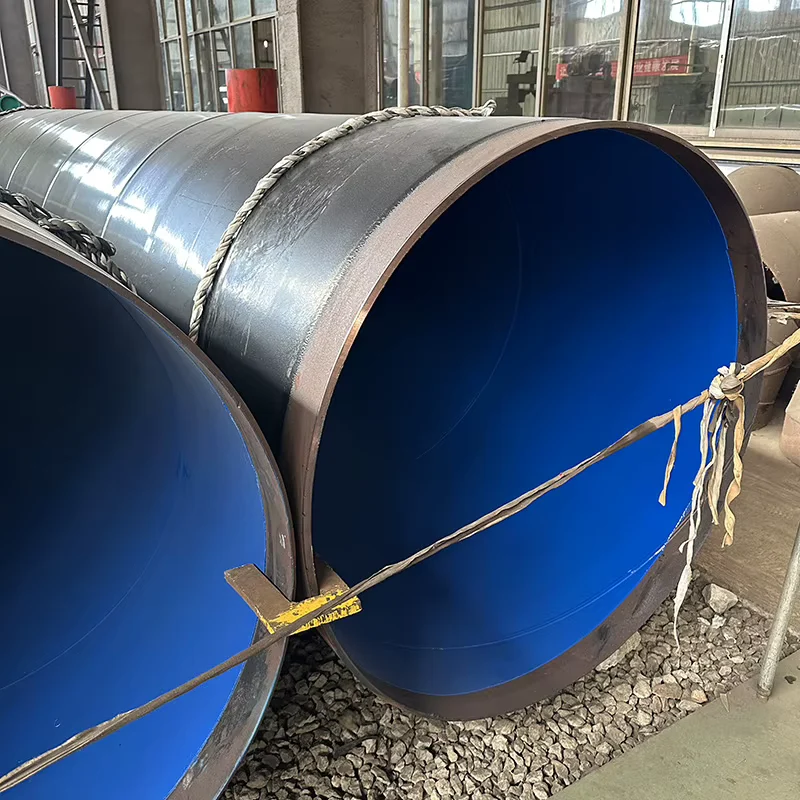
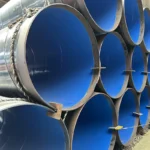
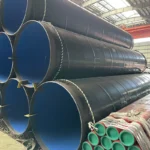
| Surface Treatment | Painting / Anti-corrosion coating / Bare / FBE / 2PE / 3PE / 3PP |
| Ends | Plain end / Beveled end / PVC covered |
| Tolerance | ±1% |
| Invoicing | By Theoretical Weight |
| Application | Piling / Heat-supply / Water conveyance / Gas transport / Mine slurry / Petroleum & natural gas / Chemical / Power engineering |
| MOQ | 25 Tons |
| Origin | Shandong, China |
Application Suitability
| Industry | Typical Applications |
|---|---|
| Infrastructure & Piling | Bridge foundation piles, port wharf steel piling, retaining wall structures |
| Municipal Engineering | Drinking water transmission mains, stormwater drainage networks, district heat-supply pipelines |
| Oil & Gas | Onshore gas gathering lines, crude oil transport pipelines, fuel gas distribution networks |
| Mining & Industrial | Mine slurry transport pipelines, chemical process piping, power plant circulating water systems |
Where Coating Adhesion Decides Whether a Water Pipeline Survives Commissioning
Submerged arc welding seams and plastic-coated surfaces must hold under hydrostatic pressure and soil stress — not just look intact at the mill gate.
I once watched a container of spiral welded pipes arrive at a Middle Eastern port where the plastic coating peeled during the customer’s adhesion bend test on site. The entire shipment sat at the depot for weeks while local crews re-coated every single pipe at triple the original cost. That kind of failure doesn’t show up in a visual inspection before loading — it shows up when the pipe bends under soil load or when the coating meets salt-laden groundwater. For any SSAW spiral welded steel pipe destined for buried water conveyance or heat-supply networks, coating integrity and weld seam quality demand verification at every production stage, not just a final glance [NEED_CITE: API 5L coating adhesion and holiday detection requirements].
Matching Large-Diameter Spiral Pipe to Buried Pipeline Engineering
When municipal engineers specify OD 600–1200 mm pipes for drinking water mains or heat-supply networks, the spiral weld geometry distributes hoop stress more evenly than straight seam alternatives under equivalent internal pressure — allowing wall thickness optimization without sacrificing structural margin. Our Q235B and Q345B grades in this diameter range ship with FBE, 2PE, or 3PE coatings selected based on soil resistivity data from the project route, and each SSAW spiral welded steel pipe leaves the mill with beveled ends ready for field welding and joint coating.
Structural Compliance and Certification for Cross-Border Pipeline Projects
Buried steel pipelines must satisfy both the mechanical demands of internal operating pressure and external soil loading, as well as the documentary requirements of the destination country’s customs and engineering approval bodies [NEED_CITE: API 5L and ASTM A53 material compliance documentation for pipeline projects]. Pipes manufactured under API 5L or GB/T9711 standards carry heat-number traceability from slab to finished pipe, while ASTM A53 and A106 designations open North American procurement channels. Surface treatment selection — bare for temporary piling, FBE for high-temperature service, 3PE for aggressive soil environments — directly determines service life and maintenance intervals. Custom cut lengths between 5.8 m and 11.8 m reduce field welding joints and accelerate installation timelines on linear pipeline routes.
Understanding Spiral Welding, Steel Grade Selection, and Coating Systems
The SSAW process forms pipe by helically winding steel coil and welding the seam via submerged arc welding, which allows production of large diameters up to 2200 mm from relatively narrow coil stock — a cost advantage over plate-based straight seam methods at bigger sizes. Under equal internal pressure, the spiral weld orientation subjects the seam to approximately 75%–90% of the hoop stress experienced by a longitudinal seam, permitting modest wall thickness reductions while maintaining equivalent pressure ratings [NEED_CITE: spiral weld stress distribution compared to straight seam pipe]. Steel grade selection follows project specification: Q195 and Q235B serve general structural and low-pressure conveyance applications, while Q345B provides higher yield strength for deeper burial or higher operating pressures. Coating systems layer differently — FBE bonds directly to blast-cleaned steel for single-layer corrosion protection, while 3PE combines an epoxy primer, adhesive copolymer, and polyethylene outer jacket for mechanical damage resistance during backfilling.
Hidden Costs When Material Traceability or Coating Quality Falls Short
A pipe that arrives without legible heat numbers on the coating surface becomes untraceable at the inspection pit — and untraceable pipe gets rejected by third-party inspectors regardless of whether the steel itself passes chemical analysis. Missing or incomplete mill test certificates cause customs holds at destination ports, turning a routine delivery into a weeks-long documentary scramble [NEED_CITE: steel pipe customs clearance documentation requirements]. Coating holidays — pinholes or thin spots invisible to the naked eye — accelerate localized corrosion under soil, leading to premature pipeline leaks and costly excavation repairs years after commissioning. These failures trace back to procurement decisions that prioritized unit price over verified certification and documented inspection.
Why Project Buyers Source SSAW Spiral Welded Steel Pipe From Our Jinan Mill
We run three simultaneous production lines with monthly capacity exceeding 20,000 tons, meaning large-diameter orders for pipeline projects don’t compete with smaller structural tube runs for mill time. Every batch of SSAW spiral welded steel pipe ships with original mill test certificates documenting chemical composition and mechanical properties per the applicable standard — API 5L, ASTM A53, or GB/T9711 as specified. Third-party inspection through SGS or BV is available on request before container sealing, giving project owners independent verification of coating thickness, weld seam quality, and dimensional accuracy. Our inventory covers over 2,800 specifications across round pipes, section steel, and plate, so consolidated multi-product container loading reduces freight cost per ton for projects needing pipe alongside beams or channels. Professional export documentation handling covers packing lists, bills of lading, and certificates of origin formatted for the destination country’s customs requirements.
Documentation & Compliance
- Mill test certificate documenting Q235B or Q345B chemical composition and mechanical properties per API 5L or GB/T9711 for each heat number
- ISO 9001:2015 quality management certificate covering the full SSAW spiral welded steel pipe production process
- SGS or BV third-party inspection report verifying coating thickness, weld seam integrity, and dimensional tolerance before shipment
- Material traceability sheet linking each pipe to its original slab heat number, chemical analysis, and rolling record
- Customs documentation package including commercial invoice, packing list, bill of lading, and certificate of origin formatted for destination port requirements
Packaging, Loading & Delivery
- Q235B and Q345B SSAW pipes bundled with steel strip bands and edge protectors to prevent coating damage during ocean transit
- FBE, 2PE, or 3PE coated pipe ends capped with PVC or steel protectors to preserve beveled edge geometry for field welding
- Container loading plans optimized for OD 219–2200 mm diameter ranges, nesting smaller pipes inside larger diameters where physically possible to maximize payload per container
- Custom cut lengths between 5.8 m and 11.8 m available to match project pipeline route segments and reduce field welding joints
- Each pipe marked with heat number, steel grade, OD, wall thickness, and length for on-site identification and traceability verification
- FOB, CIF, and DDP shipping terms available with professional export team handling documentation and port coordination
Getting Your SSAW Spiral Welded Steel Pipe Quote Started
Submit your project specifications — outer diameter, wall thickness, steel grade, coating type, total tonnage, and destination port — and receive a competitive bulk quotation within hours, complete with volume pricing and estimated production lead times. We’ll confirm mill test certificate availability, third-party inspection scheduling, and container loading optimization before you commit to a deposit, so there are no surprises between inquiry and delivery.
Frequently Asked Questions
Q: What is the difference between SSAW, LSAW, and ERW spiral welded steel pipe for pipeline projects?
A: SSAW pipe is formed by helically winding steel coil and welding via submerged arc welding, allowing large diameters up to 2200 mm from narrower coil stock. LSAW uses plate pressed and welded along a straight longitudinal seam, typically for very thick walls at large diameters. ERW uses high-frequency electric resistance welding for smaller diameters and thinner walls. The choice depends on your project’s diameter range, wall thickness, pressure rating, and budget.
Q: How do API 5L, ASTM A53, and GB/T9711 standards compare for SSAW pipe selection?
A: API 5L governs line pipe for petroleum and natural gas transportation and specifies rigorous chemical and mechanical requirements. ASTM A53 covers seamless and welded black and hot-dipped galvanized steel pipe for general mechanical and pressure applications. GB/T9711 is the Chinese national standard equivalent to ISO 3183 for petroleum and natural gas industries. We supply SSAW spiral welded steel pipe to all three standards and provide cross-reference guidance for grade equivalence.
Q: What coating system should I specify for buried water conveyance pipelines?
A: For buried water pipelines, 3PE coating (fusion-bonded epoxy primer, adhesive copolymer, and polyethylene outer layer) provides the best combination of corrosion protection and mechanical resistance during backfilling. FBE single-layer coating suits high-temperature service or less aggressive soil conditions. The choice depends on soil resistivity data, operating temperature, and installation conditions along your pipeline route.
Q: Can I request third-party inspection before my SSAW pipe shipment loads?
A: Yes. SGS and BV third-party inspections are available on request and cover coating thickness measurement, weld seam visual and ultrasonic examination, dimensional verification, and hydrostatic testing where applicable. The inspection occurs at our mill before container sealing, and the report is included in your shipping documentation package.
Q: How is SSAW spiral welded steel pipe invoiced — by actual weight or theoretical weight?
A: Our SSAW pipe is invoiced by theoretical weight calculated from the specified outer diameter, wall thickness, and length, with a dimensional tolerance of ±1%. This is the standard industry practice for welded steel pipe and ensures transparent pricing independent of minor manufacturing weight variations.
Request Your SSAW Spiral Welded Steel Pipe Quotation Today
Send your project specifications — diameter, wall thickness, steel grade, coating, quantity, and destination — to receive factory-direct pricing with mill test certificates and third-party inspection options included.
Shandong Xin Jiyuan Special Steel Tube Co., Ltd
Website: www.sdxinjiyuan.com
Tel: +86 531 8573 6315
Mobile/WhatsApp/WeChat: +86 188 5315 7756
Email: admin@sdxinjiyuan.com
Address: No.11889, Jingshi West Road, Lulian Group, Jinan City, Shandong Province, China