

Description
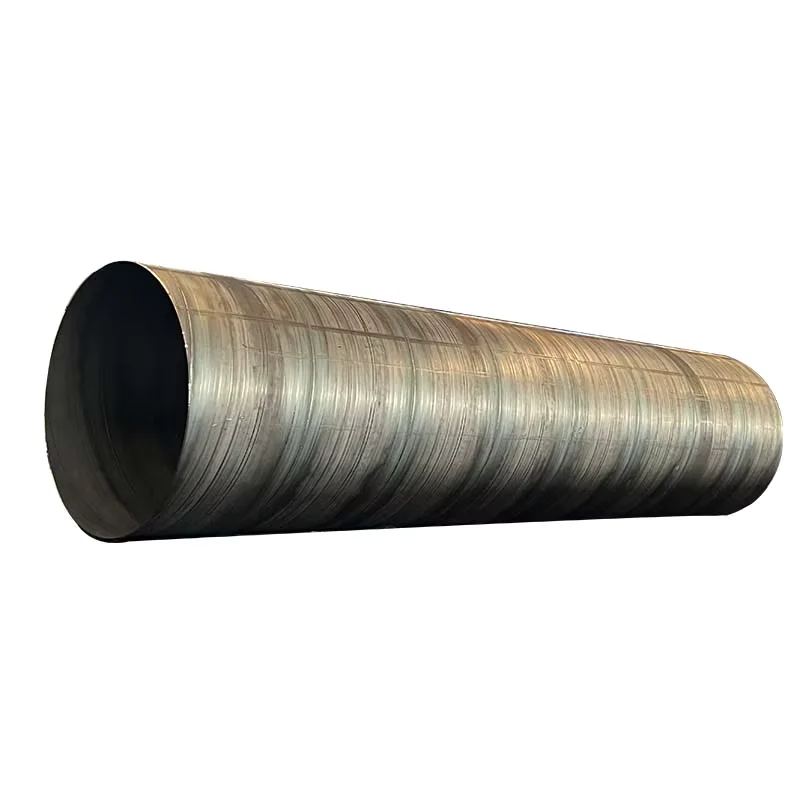
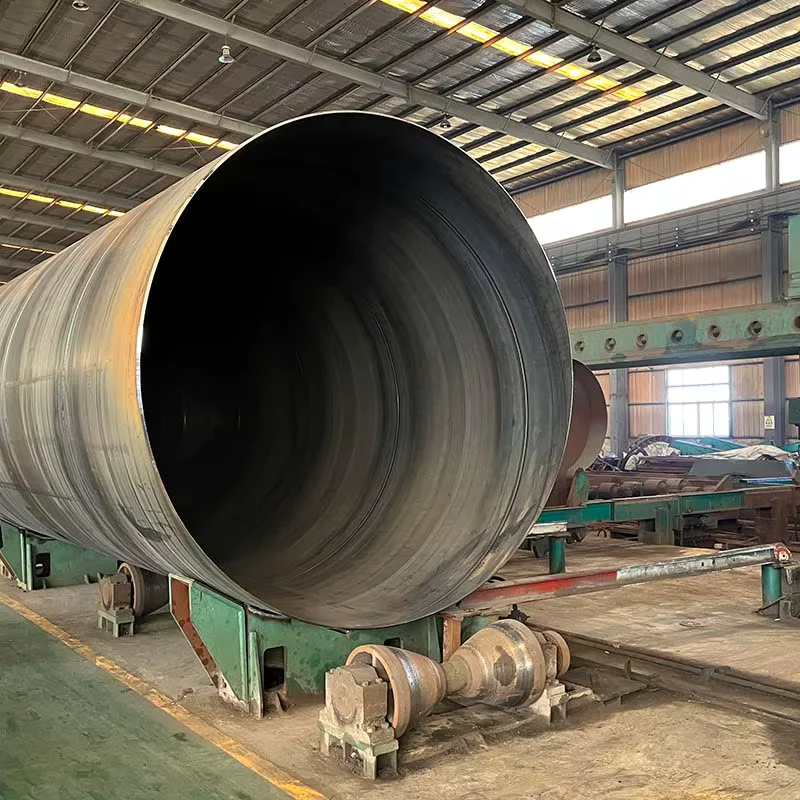
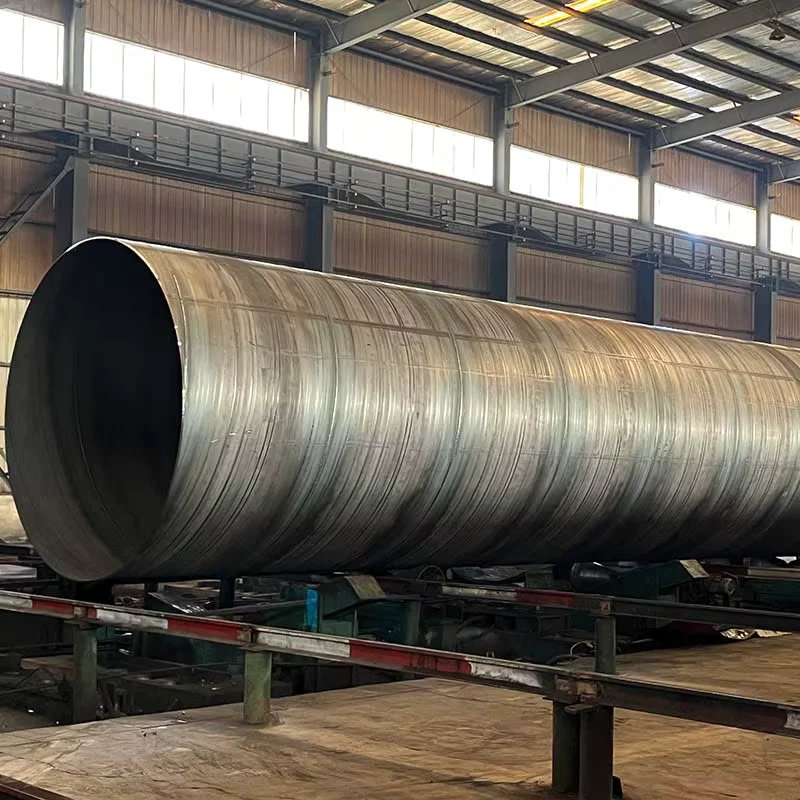
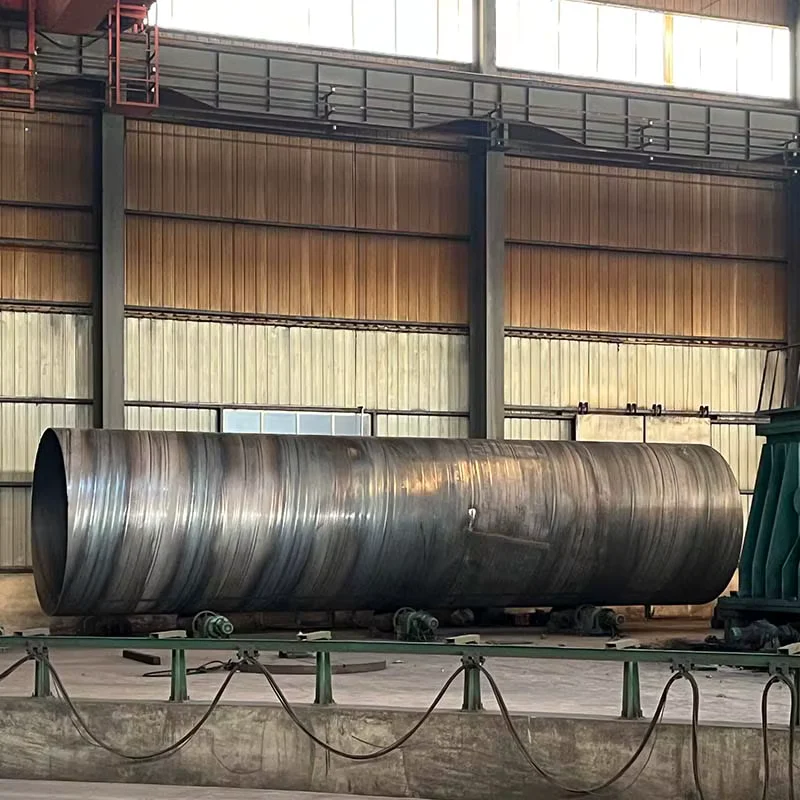
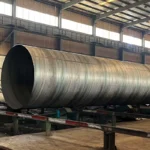
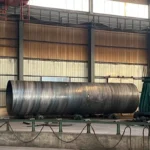
Factory-direct SSAW pipe mill — every spiral-welded order rolls through our own UT and PMI stations before container sealing, eliminating third-party markup and certification gaps.
Technical Specifications
| Parameter | Value |
|---|---|
| Designation | ASTM A106/A53 Gr.B SSAW Steel Pipe |
| Product Type | SSAW Steel Pipe / Spirally Submerged Arc Welded Pipe |
| Steel Grade | Q195, Q215, X42, X46, L242, L450, ASTM A106/A53 Gr.B |
| Standard | API, ASTM A106, ASTM A53, CE, JIS |
| Section Shape | Round |
| Size Range | OD 400–3000 mm (15.75–118.11 in) |
| Length | 6m / 12m |
| Technique | SSAW (Spirally Submerged Arc Welding) |
| Surface Treatment | Black Painted / Oiled / Anti-corrosion coating |
| Tolerance | ±1% |
| Ends | Plain / Beveled |
| Application | Gas pipeline / Oil pipeline / Fluid transport / Structural piling / Water transmission |
| MOQ | 1 Ton |
| Origin | Shandong, China |
Application Suitability
| Industry | Typical Applications |
|---|---|
| Oil & Gas EPC | Long-distance transmission pipelines, gathering lines, compressor station piping |
| Municipal Infrastructure | Raw water intake mains, treated water distribution trunk lines, drainage outfalls |
| Civil & Port Engineering | Bridge foundation piling, wharf sheet pile backing, offshore platform jacket legs |
| Industrial Plant | Cooling water circulation loops, slurry transport lines, process fluid headers |
Where Third-Party Re-Inspection Exposes Buried Weld Defects on Large-Diameter Pipe
A mill UT pass does not guarantee field acceptance — spiral weld porosity hidden beneath slag inclusions only surfaces when the client’s independent lab re-scans at the job site.
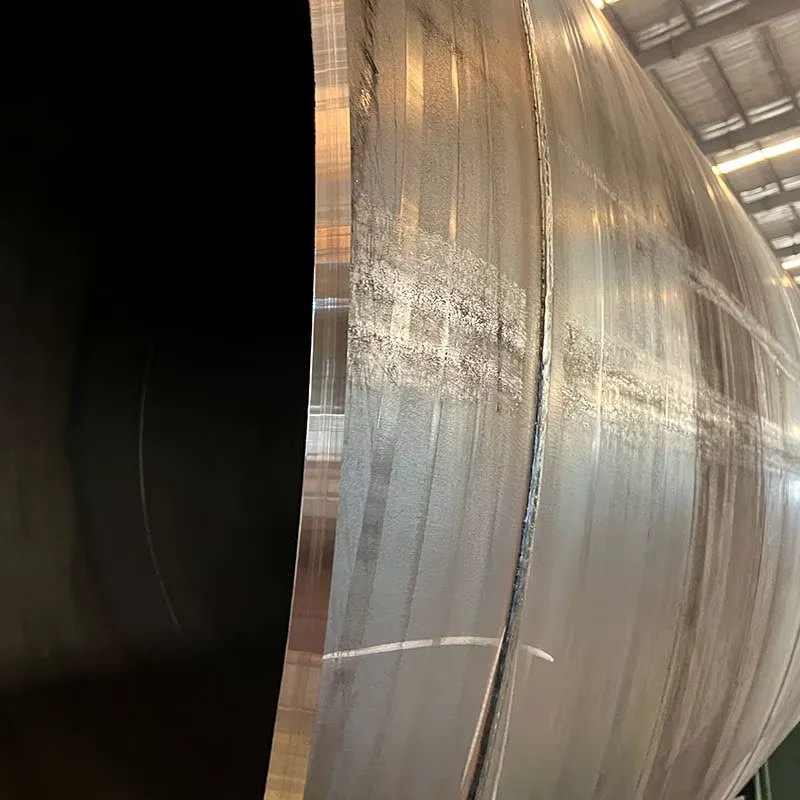
Sourcing large-diameter welded pipe from fragmented suppliers often means receiving mill certificates that look clean on paper but fail re-inspection under stricter project-spec scanning protocols. Trace porosity buried deep in the spiral seam, incomplete fusion at the weld-to-base-metal junction, or hydrogen-induced cracking from improper preheat — these defects pass basic mill UT but collapse under API 5L supplementary requirements or client-mandated phased-array imaging. Two containers sitting at a Middle Eastern port for three weeks while replacement pipe is scrambled is not a logistics problem; it is a process-control failure that no amount of paper certification can cover. Every SSAW steel pipe manufacturer claiming API compliance should demonstrate full spiral weld UT coverage and positive material identification before loading, not just stamp a certificate at the gate. [NEED_CITE: API 5L supplementary requirement U2 ultrasonic testing coverage for spiral welded pipe]
Matching OD 400–3000mm Spiral-Welded Pipe to Pipeline and Piling Service Conditions
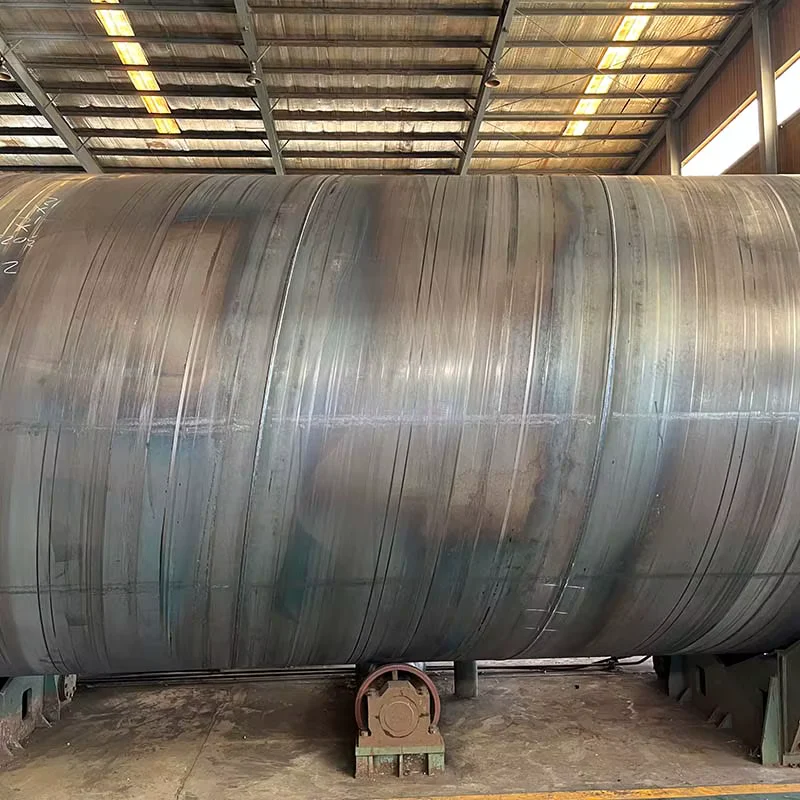
Large-diameter SSAW steel pipe fills the gap between ERW lines (typically limited to OD 610mm) and LSAW mills (economical above OD 508mm but with higher per-ton cost on long runs). The spiral forming process allows continuous production across the full 400–3000mm OD range from a single coil width, making it the default choice for municipal water transmission mains in the 800–1600mm range and structural piling in the 1000–2400mm range. For oil and gas transmission, API-grade X42 and X46 coils are formed under controlled tension with inline seam tracking, then submerged-arc welded from both inside and outside simultaneously to ensure full-penetration fusion across the spiral seam. The SSAW steel pipe manufacturer must verify weld seam integrity through 100% automated UT before hydrostatic testing — a step that separates project-grade supply from commodity trading stock.
Engineering Code Compliance and Corrosion Environment Selection
Structural piling applications require the pipe to meet driving stress limits under EN 1993-5 or AISC 360, which means wall thickness tolerance directly affects section modulus calculations — a ±1% tolerance on OD combined with tight wall control ensures the as-delivered section modulus stays within design assumptions. For buried water transmission lines in aggressive soil conditions, the black painted or oiled surface provides short-term transit protection, but long-term service demands 3PE or FBE anti-corrosion coating applied after welding — a specification the buyer must confirm at inquiry stage, not after the pipe reaches the trench. Certification alignment matters at customs: CE-marked pipe under EN 10210/10219 clears EU ports without re-inspection delay, while ASTM A106/A53 Gr.B documentation satisfies North American EPC procurement systems. [NEED_CITE: EN 10219 cold-formed welded structural hollow sections dimensional tolerance requirements]
Steel Grade Selection and Spiral Welding Process Fundamentals
The Q-series grades (Q195, Q215) serve low-pressure water and drainage applications where formability matters more than yield strength, while the API 5L grades (X42, X46, L242, L450) are specified for pressurized hydrocarbon transmission where the minimum yield strength designation directly determines the design pressure rating under ASME B31.4 or B31.8. ASTM A53 Gr.B bridges both worlds — accepted for structural piling and low-pressure fluid conveyance, with chemical composition compatible with standard welding procedures without preheat on thinner walls. The SSAW process itself uses a continuously advancing strip fed at a controlled angle to the pipe axis, creating the spiral seam — this geometry allows a single strip width to produce multiple ODs, but also means the weld seam experiences combined tensile and shear stress during hydrostatic proof testing, requiring dual-sided submerged-arc welding with real-time seam tracking. Surface treatment selection follows service environment: oiled finish for indoor structural use, black painted for temporary outdoor exposure, and anti-corrosion coating (3PE, FBE, or coal tar enamel) for buried or submerged installation. Wall thickness tolerance of ±1% ensures the actual weight per meter stays within invoicing accuracy, while the ±1% OD tolerance maintains fit-up compatibility with standard flanges and coupling systems.
The Hidden Cost of Accepting Paper Certificates Without Process Verification
When a project specifies API X46 for a sour-service gas line and the delivered pipe carries only a generic “equivalent grade” certificate without heat-by-heat chemistry, the downstream cost is not the pipe price difference — it is the NACE MR0175 compliance gap that forces the entire batch to be rejected at the welding stage. Missing CE documentation on a shipment bound for Rotterdam means customs holds the container for independent classification, adding demurrage and re-routing costs that exceed the original freight savings from choosing a cheaper supplier. Negative tolerance abuse on wall thickness — where the actual wall falls below the minimum specified under EN 10219 or API 5L — does not show up during visual inspection but reduces the pressure rating and section modulus below design assumptions, creating latent structural risk that only surfaces during hydrotest or years into service. [NEED_CITE: API 5L heat number traceability and MTC requirements for line pipe]
Why Project Buyers Source SSAW Pipe Directly From Our Mill
Every coil received into our yard is verified against the mill’s chemistry report before being released to the forming line — no blend-down, no grade substitution, no certificate swapping from trading stock. Our three production lines running simultaneously deliver monthly capacity exceeding 20,000 tons, meaning a 500-ton order for an 800mm OD water main does not compete with a 2,000mm piling job for mill time. The in-house lab conducts three-stage inspection: raw material chemistry verification before forming, in-process weld seam UT and visual check during welding, and final dimensional survey plus surface inspection before coating. For buyers consolidating a multi-category project — pipe, plate, H-beam, and fabrication — we load everything into shared containers with professional weight distribution plans, eliminating the coordination overhead of managing four separate suppliers. Original mill test certificates travel with every shipment, and SGS or BV third-party inspection is arranged on request before container sealing — not as an afterthought, but as a standard checkpoint in the release protocol.
Documentation & Compliance
- Mill test certificate documenting ASTM A106/A53 Gr.B chemical composition and mechanical properties per heat number, issued from the original coil producer
- CE certificate covering EN 10210/10219 compliance for structural hollow sections exported to European Economic Area markets
- ISO 9001:2015 quality management certificate covering the full SSAW production process from coil intake to finished pipe dispatch
- SGS or BV third-party inspection report verifying dimensional tolerance, weld seam UT results, and surface coating thickness before container loading
- Material traceability report linking each pipe length to its heat number, coil identity, and production date for project quality file submission
- Export documentation package including packing list, bill of lading, certificate of origin, and fumigation certificate for customs clearance at destination port
Packaging, Loading & Delivery
- SSAW pipe bundled with high-tensile steel strips at intervals matching the 6m/12m length, with end protectors on beveled-end pipes to preserve weld preparation geometry during ocean transit
- Black painted or oiled surface wrapped with waterproof cloth at pipe ends to prevent moisture ingress and coating damage during container loading and unloading
- Container loading plan optimized for OD 400–1200mm pipe nested inside larger OD 1200–2400mm pipe to maximize weight utilization per 40ft open-top or flat-rack container
- Custom cut-length service available for 6m and 12m standard lengths, with saw-cut precision matching the ±1% tolerance for direct field weld-fit without secondary machining
- Heat number and steel grade stenciled on each pipe length at 1-meter intervals for site identification and traceability verification during installation
- FOB, CIF, and DDP shipping terms available with professional export team handling customs declaration, port coordination, and real-time container tracking through to project site delivery
Submit Specifications to Receive Factory-Direct Pricing and Mill Test Certificates
Project procurement teams and pipeline EPC contractors should submit pipe specifications — including OD, wall thickness, length, steel grade, quantity, and destination port — to receive a detailed quotation with volume-based pricing, production lead time, and sample mill test certificate for quality verification. Non-standard specifications, custom coating requirements, and consolidated multi-product container loading plans are confirmed during the technical review stage before contract signing.
Request Your SSAW Pipe Quotation and Material Documentation
Send your specification sheet to admin@sdxinjiyuan.com or contact via WhatsApp at +86 188 5315 7756 for response within 12 hours with pricing, MTC sample, and delivery schedule.