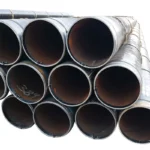
Description
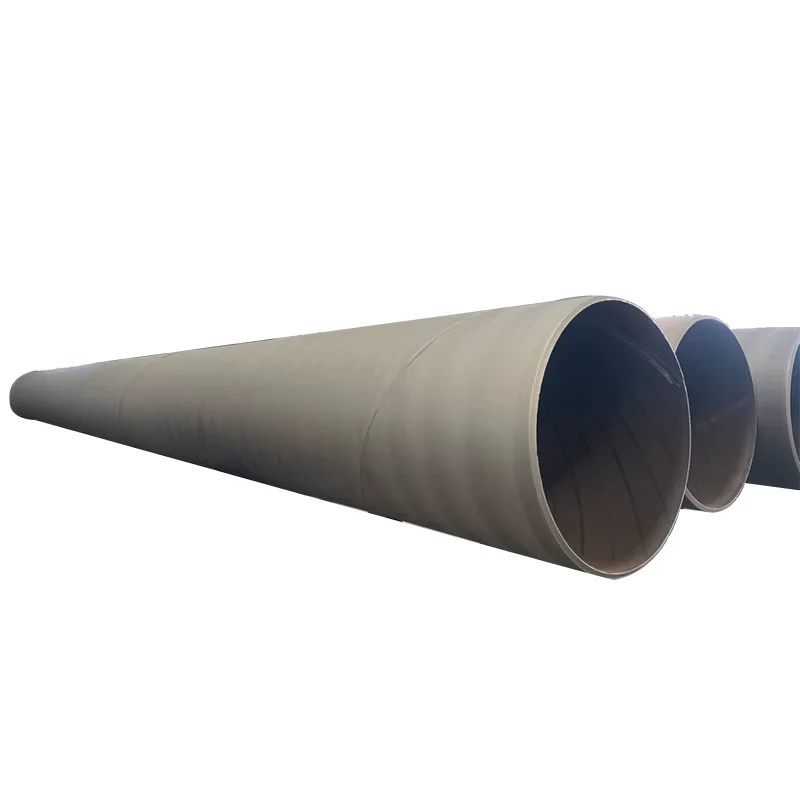
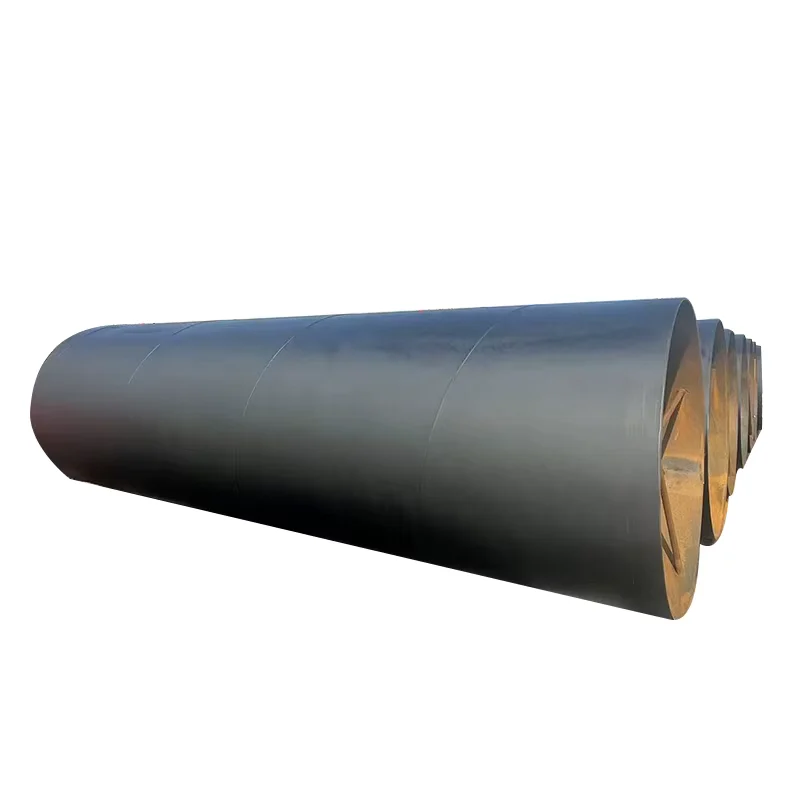
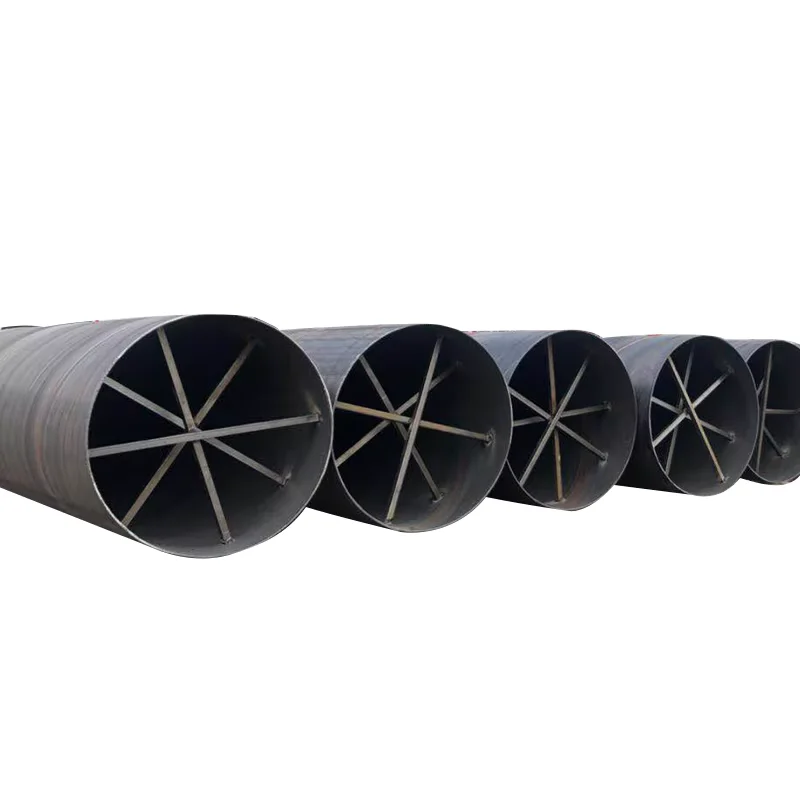
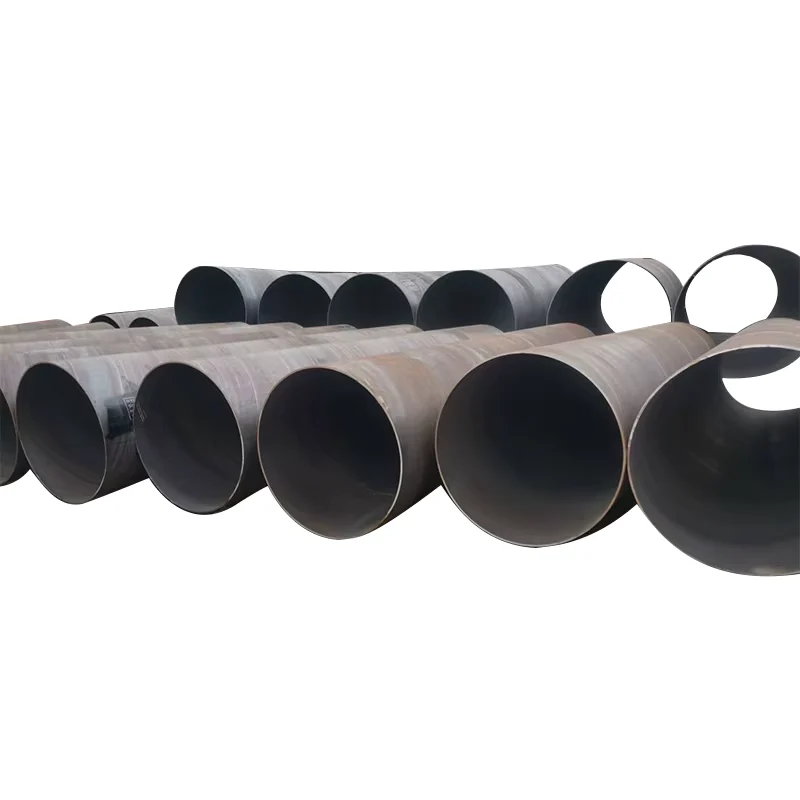
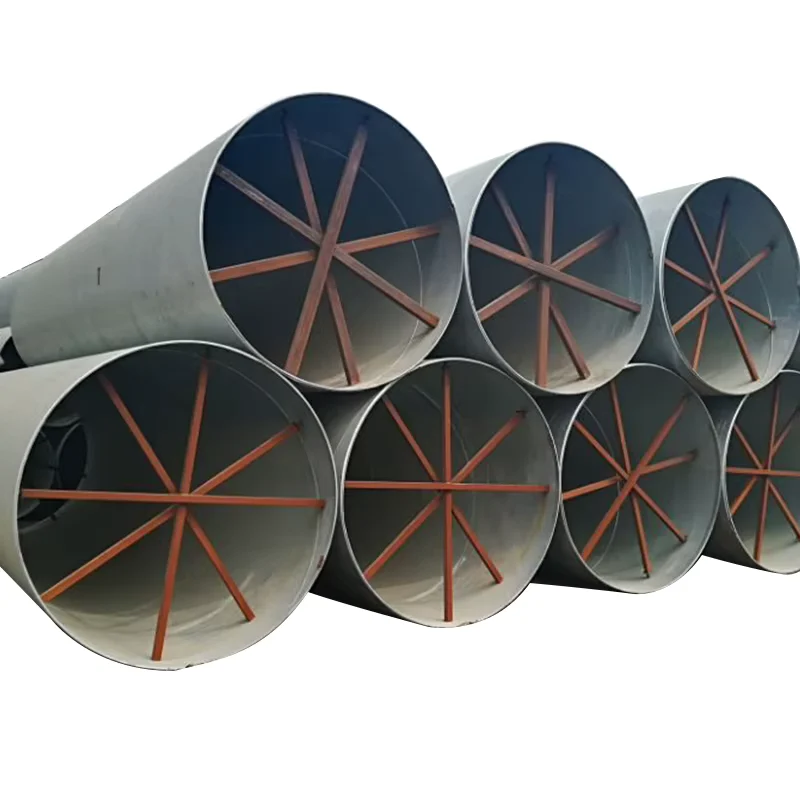
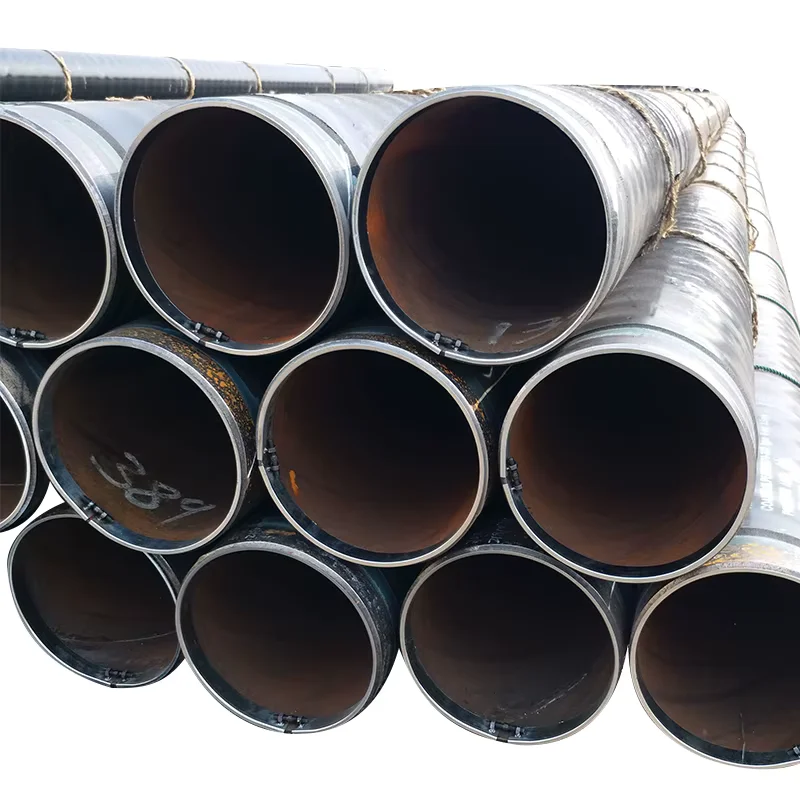
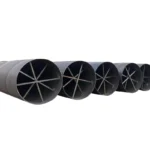
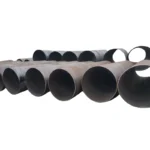
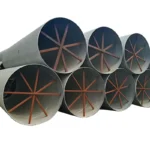
Factory-direct SSAW pipe — 3 production lines producing API 5L and EN 10219 grades in OD 219.1–4064 mm with original mill certificates on every heat.
Technical Specifications
| Parameter | Value |
|---|---|
| Designation | SSAW Steel Pipe |
| Product Type | Spiral Submerged Arc-Welded Pipe |
| Steel Grade | API 5L (A, B, X42, X46, X52, X56, X60, X65, X70), ASTM A53 Gr. A/B, ASTM A252 (Gr.1/2/3), EN 10219 (S235JR, S275JR, S355JR, S355JOH, S355J2, S420), GB/T9711 (L175–L555), Q195–Q345 |
| Standard | API 5L PSL1/PSL2, ASTM A252, ASTM A53, EN 10219, AWWA C200, GB/T9711, BS, JIS |
| Section Shape | Round |
| Size Range | OD 219.1 mm – 4064 mm (8″ – 160″) |
| Wall Thickness | 4 mm – 25.4 mm |
| Length | Up to 96 m (standard 6 m / 12 m) |
| Technique | SSAW (Spiral Submerged Arc Welding) |
| Surface Treatment | Anti-rust coating, Bitumen coating, FBE, 2PE, 3LPE, Polyamide Epoxy, Rich Zinc Primer, Polyurethane |
| Ends | Plain / Beveled |
| Tolerance | ±10% |
| Application | Oil and gas transmission, water supply, urban heating, sewage discharge, steel structure, bridges, foundation piling, port machinery, electrical power |
| MOQ | 1 Ton |
| Origin | Shandong, China |
Application Suitability
| Industry | Typical Applications |
|---|---|
| Oil & Gas / Energy | Onshore and offshore transmission pipelines, gathering lines, slug catchers |
| Municipal Infrastructure | Raw water conveyance mains, district heating networks, stormwater and sewage outfalls |
| Civil Engineering & Foundations | Bridge pier casings, bored pile sleeves, sheet pile anchor tubes |
| Industrial & Port | Conveyor support columns, crane booms, wharf fender piles |
Where Missing API 5L Certification Halts a Pipeline Project at Customs
A pipe without a verifiable heat number and matching mill test certificate is scrap metal at the port.
Global buyers routinely face customs holds because the supplier’s paperwork does not trace back to the specific heat of steel rolled. On SSAW steel pipe projects governed by API 5L PSL2, the importing country’s petroleum authority will reject the shipment if the chemical composition and mechanical test results cannot be matched to the pipe’s stamped heat code. Beyond customs, inconsistent weld seam quality — particularly lack-of-fusion defects in the spiral weld — forces costly field repairs or full line replacement. [NEED_CITE: API 5L PSL2 mandatory testing and traceability requirements]
Matching Large-Diameter SSAW Pipe to Pressure and Structural Demands
The helical weld geometry of SSAW steel pipe allows production of OD up to 4064 mm from narrower coil stock, making it the economical choice for water transmission and piling where straight-seam alternatives would require prohibitively wide plate. For oil and gas transmission in API 5L X52 through X70 grades, the spiral seam must pass 100% ultrasonic testing per API 5L Annex H, ensuring weld integrity across the full helical length. Our three production lines run simultaneous welding heads with real-time seam tracking, and every coil is verified against its mill certificate before forming — a discipline learned the hard way after an early export shipment failed third-party weld fusion inspection.
Engineering Compliance Across API, EN, and ASTM Frameworks
SSAW steel pipe supplied under API 5L PSL2 must satisfy Charpy impact testing at project-specified temperatures, a requirement that distinguishes PSL2 from PSL1 and directly affects material selection for sub-zero or offshore environments. For foundation piling to ASTM A252, the pipe’s spiral seam orientation must be documented in the mill test certificate to confirm compliance with allowable stress assumptions in geotechnical design. In European markets, EN 10219 structural hollow sections demand CE marking and factory production control audits — certificates we hold and provide with each shipment. [NEED_CITE: EN 10219 cold-formed structural hollow section compliance] Wall thickness tolerance of ±10% means procurement teams must calculate section modulus using minimum wall, not nominal, to avoid under-design in load-bearing applications.
Understanding Steel Grade Selection and Spiral Welding Mechanics
API 5L grade progression from B through X70 reflects increasing minimum yield strength, with X65 and X70 specified for high-pressure gas transmission where wall thickness optimization reduces total tonnage and welding cost. EN 10219 grades S235JR through S420 serve structural applications where impact toughness at sub-zero temperatures (JOH, J2 designations) governs selection over pure strength. The SSAW process forms coil into a helix at a controlled angle, enabling large diameters from standard-width plate — this geometry distributes welding heat input more evenly than longitudinal seam processes but demands precise flux coverage and seam tracking to avoid porosity or slag inclusion. Surface treatment selection follows environment: FBE coating provides chemical resistance for buried pipelines, 3LPE adds mechanical protection for rocky backfill, and bitumen coating serves cost-effective corrosion protection in non-aggressive soils. [NEED_CITE: SSAW versus LSAW manufacturing process comparison]
The Hidden Cost of Unverified Wall Thickness and Missing Certificates
Purchasing SSAW steel pipe at the lowest quoted price often means accepting negative tolerance beyond the ±10% standard, reducing actual wall thickness and compromising pressure rating or structural load capacity. When a project engineer discovers that delivered pipe weight falls below theoretical weight by more than the allowable tolerance, the entire batch may be rejected — forcing air freight replacement or project delay penalties that dwarf the initial price saving. Missing CE or API certificates do not just delay customs; they invalidate the engineer’s design certification, requiring complete re-submission to the authority. [NEED_CITE: steel pipe tolerance standards and weight calculation methods]
Procurement Confidence Built on Traceable Production
Every SSAW steel pipe order ships with original mill test certificates listing chemical composition and mechanical properties per the specified standard, traceable by heat number to the coil source. Our in-house laboratory conducts three-stage inspection — incoming coil chemistry, in-process weld parameters, and finished pipe hydrostatic testing — with SGS or BV third-party inspection available for clients requiring independent verification. The factory-direct model eliminates trading margins, and volume discount programs reward long-term partnerships with recurring procurement. We consolidate multi-product shipments, loading SSAW pipe alongside plate, beam, and section steel in optimized container configurations that reduce per-ton freight cost. Custom lengths up to 96 m and non-standard diameters are produced on dedicated lines with typical lead times of 15–25 days, while standard specifications ship from ready stock.
Documentation & Compliance
- Mill test certificate documenting API 5L X52 chemical composition, yield strength, and tensile properties per heat number
- CE certificate confirming EN 10219 compliance for structural hollow sections exported to European markets
- ISO 9001:2015 quality management certificate covering the full SSAW production process
- SGS or BV third-party inspection report verifying wall thickness, weld seam ultrasonic testing, and coating adhesion
- Material traceability sheet linking each pipe’s heat number to coil chemistry and rolling records
- Export documentation package including packing list, bill of lading, and certificate of origin for customs clearance
Packaging, Loading & Delivery
- SSAW steel pipe bundled with galvanized steel strips at intervals calculated for OD and wall thickness to prevent ovalization during ocean transit
- Beveled ends protected with plastic caps to preserve welding preparation and prevent moisture ingress
- 3LPE and FBE coated pipe wrapped with abrasive-resistant cloth to prevent coating damage from handling equipment
- Container loading plans optimized for 12 m and 6 m standard lengths, maximizing payload while respecting road weight limits at destination
- Each pipe stenciled with heat number, steel grade, OD, wall thickness, and standard designation for site identification
- FOB, CIF, and DDP terms available with professional customs documentation and port coordination
Request Your SSAW Steel Pipe Quotation with Mill Certificates
Submit your specification sheet listing OD, wall thickness, length, steel grade, quantity, and destination port to receive a competitive bulk quotation within 12 hours, complete with mill test certificate samples and third-party inspection options. Our engineering team will confirm standard stock availability or provide a production schedule for custom diameters and non-standard lengths.
Start Your SSAW Steel Pipe Inquiry
Send your requirements by email to admin@sdxinjiyuan.com or contact us via WhatsApp at +86 188 5315 7756 to receive pricing, mill test certificates, and delivery schedules for your next project.
Frequently Asked Questions
Q: What is the difference between SSAW, LSAW, and ERW pipe for my project?
A: SSAW steel pipe uses spiral submerged arc welding to produce large diameters from narrower coil, making it cost-effective for water transmission and piling. LSAW uses longitudinal seam welding on plate, preferred for high-pressure oil and gas. ERW produces smaller diameters with high-speed electric resistance welding for structural and low-pressure applications.
Q: Can you provide API 5L X65 SSAW pipe with PSL2 requirements?
A: Yes, we produce API 5L grades from A through X70 in both PSL1 and PSL2, with PSL2 including mandatory Charpy impact testing, hydrostatic testing, and 100% weld seam ultrasonic inspection per API 5L Annex H.
Q: What surface treatment is best for buried pipelines in corrosive soil?
A: For aggressive soil conditions, 3LPE coating provides both chemical resistance and mechanical protection against rock impingement. FBE coating offers excellent chemical resistance for less abrasive environments, while bitumen coating serves as a cost-effective solution for non-aggressive soils.
Q: What is the minimum order quantity and can you produce custom lengths?
A: Our MOQ is 1 ton for trial orders, with standard lengths of 6 m and 12 m from ready stock. Custom lengths up to 96 m are available with typical production lead times of 15–25 days.
Q: Do you provide third-party inspection and certification for EU markets?
A: Yes, we hold CE certification for EN 10219 structural hollow sections and ISO 9001:2015 quality management. SGS and BV third-party inspection is available on request, with original mill test certificates provided for every heat.