
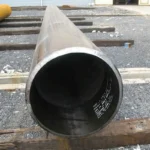
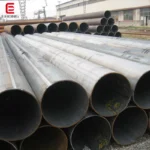
Description
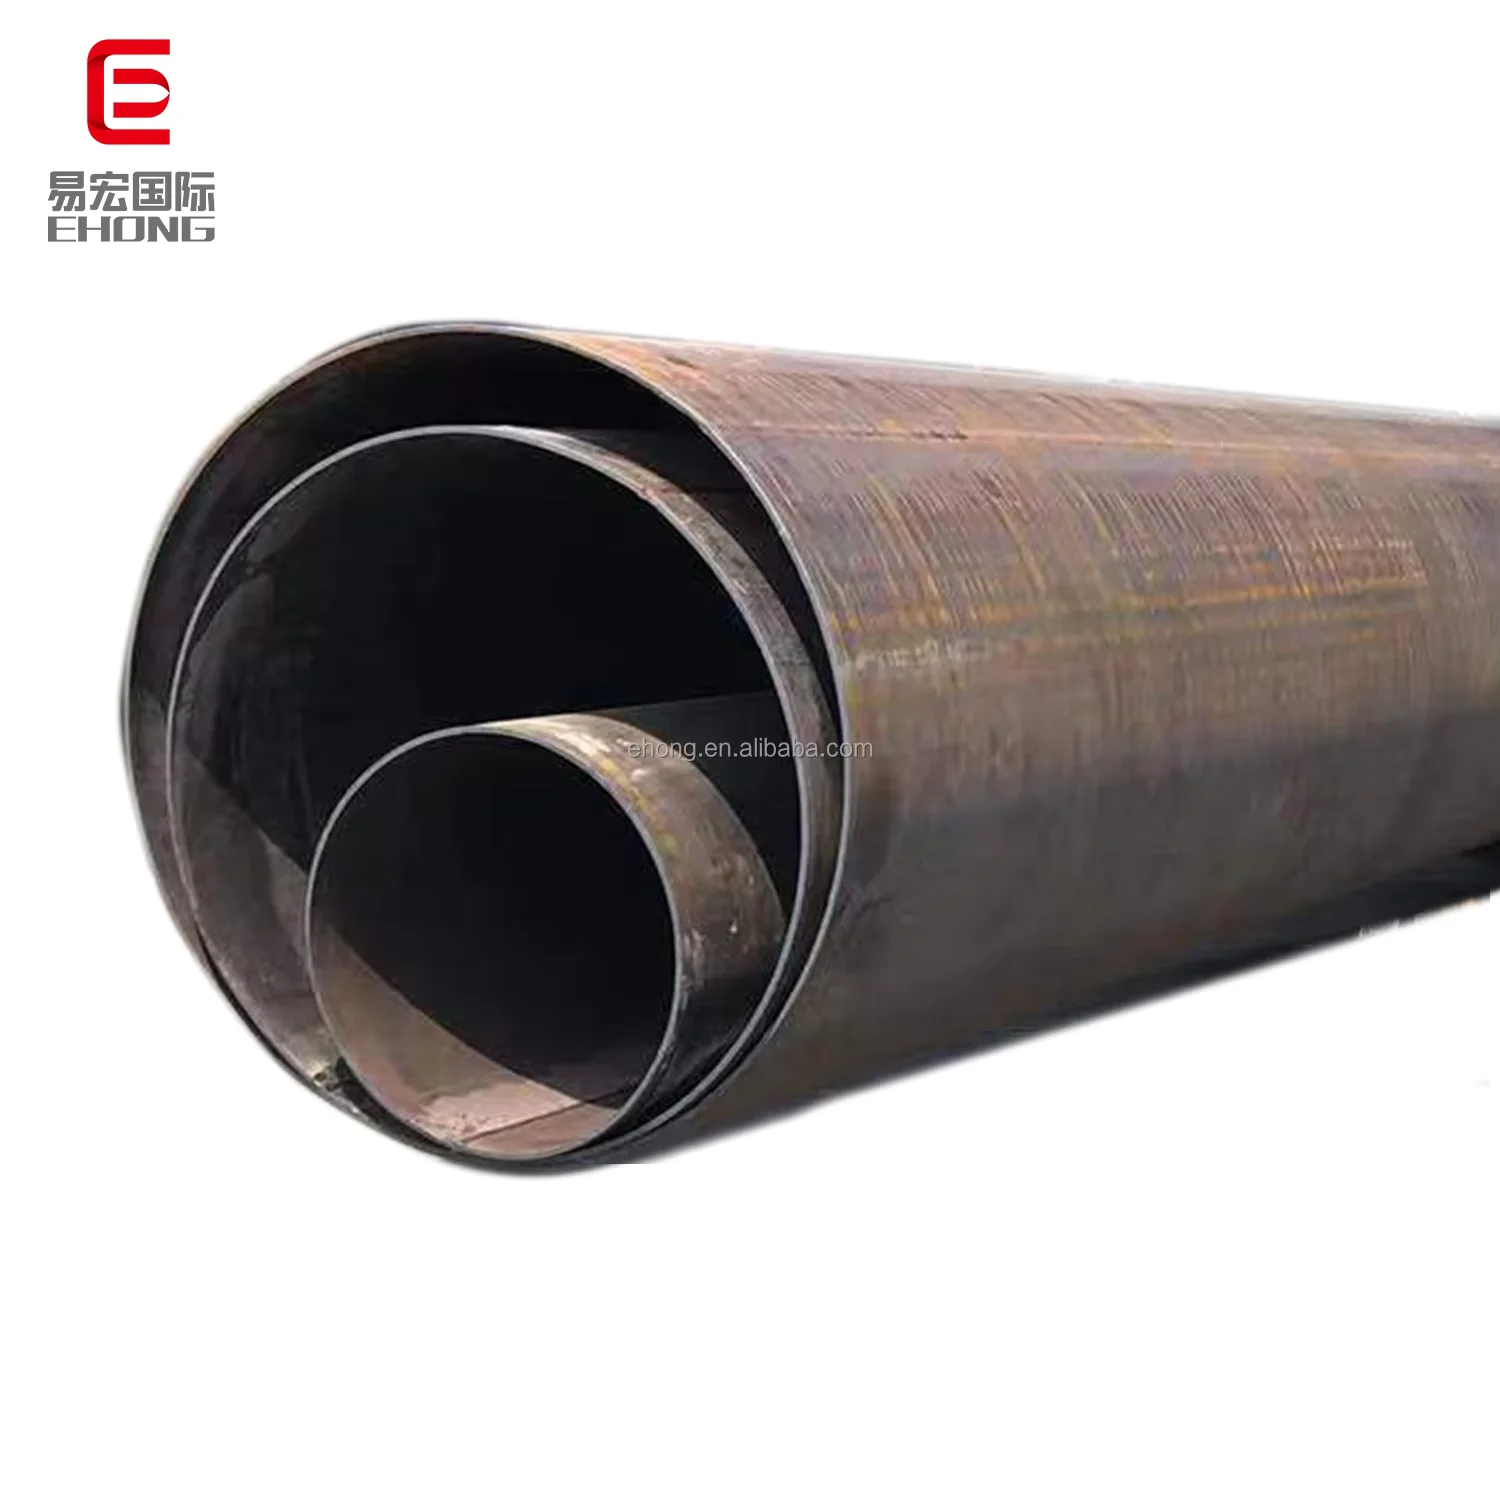
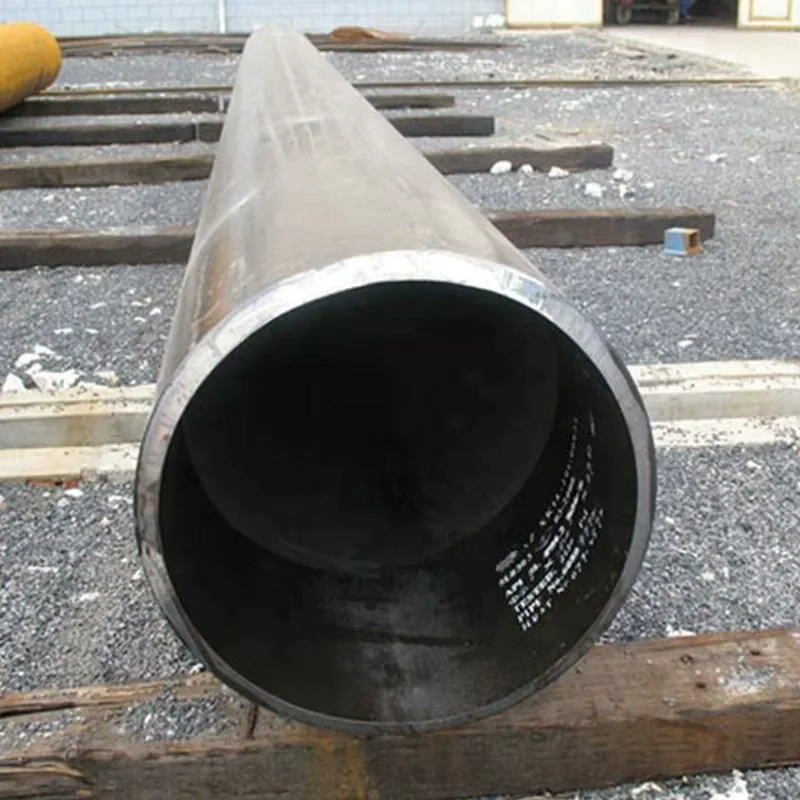
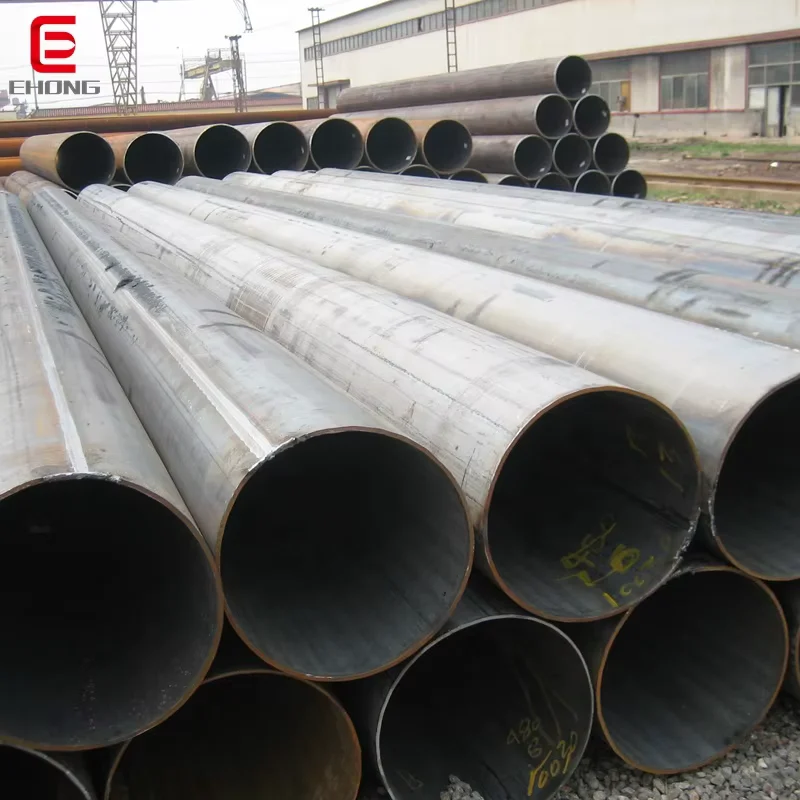
Factory-Direct LSAW Pipe Mill — Every Q235B and API 5L LSAW welded steel pipe rolls off our own submerged arc welding lines in Jinan, shipped with original mill test certificates and no trading markup.
Technical Specifications
| Parameter | Value |
|---|---|
| Designation | LSAW Welded Steel Pipe |
| Product Type | Round Steel Pipe (Longitudinal Submerged Arc Welded) |
| Steel Grade | Q235B, S235JR, S235JOH, SS400, A36, A500 Gr.A / Gr.B / Gr.C, S235, S275, S355, Q195, Q235, Q345 |
| Standard | EN10255, EN10219, EN10210, EN39, BS1387, ASTM A53, ASTM A500, ASTM A36, API 5L, ISO 65, JIS G3444, DIN 3444, ANSI C80.1, AS 1074, GB/T 3091 |
| Section Shape | Round |
| Size Range | OD 406–1524 mm |
| Wall Thickness | 8–60 mm |
| Length | 3–12 m (customizable) |
| Technique | LSAW (Longitudinally Submerged Arc Welding) |
| Surface Treatment | Oil, Black Paint, Varnish Lacquer, Epoxy Painting, FBE Coating, 3PE Coating |
| Pipe End | Plain End / Bevel End |
| Tolerance | ±1% |
| Application | Fluid transport (liquid & gas), oil pipeline, structural pipe, large-diameter long-distance transmission, infrastructure projects |
| MOQ | 1 Ton (trial order supported via LCL) |
| Origin | Shandong, China |
Application Suitability
| Industry | Typical Applications |
|---|---|
| Oil & Gas Transmission | Long-distance crude oil and natural gas pipelines, gathering lines, trunk transmission mains |
| Municipal Infrastructure | Raw water conveyance mains, industrial cooling water circuits, drainage and stormwater outfalls |
| Structural & Civil Engineering | Bridge pier casings, piling sleeves, industrial platform columns, heavy-load support frames |
| Power & Energy | Coal ash slurry lines, boiler feed water circuits, wind farm foundation monopole sections |
What Wall-Thickness Tolerance Costs on a Large-Diameter LSAW Order
A few millimeters of unchecked negative tolerance on a 1524 mm OD pipe can void an entire pipeline hydrostatic test.
When buyers source LSAW welded steel pipe from fragmented suppliers, the most common failure point is not the steel grade itself — it is the wall thickness drifting below minimum specified values across long production runs. On high-pressure oil and gas transmission lines, this means hydrostatic test failures at the commissioning stage, pipe-by-pipe re-inspection by third-party surveyors, and weeks of delay on an EPC schedule that was already tight. [NEED_CITE: API 5L dimensional tolerance requirements for line pipe] Certification gaps compound the problem: without a verifiable mill test certificate tied to a specific heat number, customs authorities in importing countries can hold the entire shipment, regardless of whether the physical product is sound.
Matching Large-Diameter LSAW Pipe to High-Pressure Transmission Lines
An LSAW welded steel pipe in the 406–1524 mm OD range with wall thickness up to 60 mm is engineered for applications where ERW pipes reach their practical limit — long-distance fluid and gas transmission under sustained internal pressure. The longitudinal submerged arc welding process produces a full-penetration weld seam with toughness properties that match or exceed the parent plate, which is why API 5L and EN10210 specifications call for LSAW on trunk pipelines. For our EPC buyers across Africa and the Middle East, we supply these pipes in 12 m random lengths with bevel ends ready for field girth welding, reducing on-site joint counts and welding time per kilometer of laid pipe.
Engineering Compliance and Corrosion Protection for Buried and Submerged Service
Large-diameter LSAW pipes serving buried water mains or offshore-adjacent structures face two simultaneous demands: structural compliance with load-bearing codes and long-term corrosion resistance. Surface treatment selection — 3PE coating for buried oil and gas lines, FBE for high-temperature service, epoxy painting for industrial fluid circuits — is decided by the operating environment, not by the pipe mill alone. [NEED_CITE: EN 10210 structural hollow section compliance requirements] Steel grade selection between Q235B, S275, and S355 directly affects the design wall thickness under internal pressure calculations per ASME B31.3 or EN 13480, and the mill test certificate must document both chemical composition and mechanical properties against the correct standard. For European market projects, CE certification under EN10210 / EN10219 is required for customs clearance; for North American buyers, ASTM A53 or API 5L grade designation must appear on all shipping documents.
Steel Grade Selection and Submerged Arc Welding Metallurgy
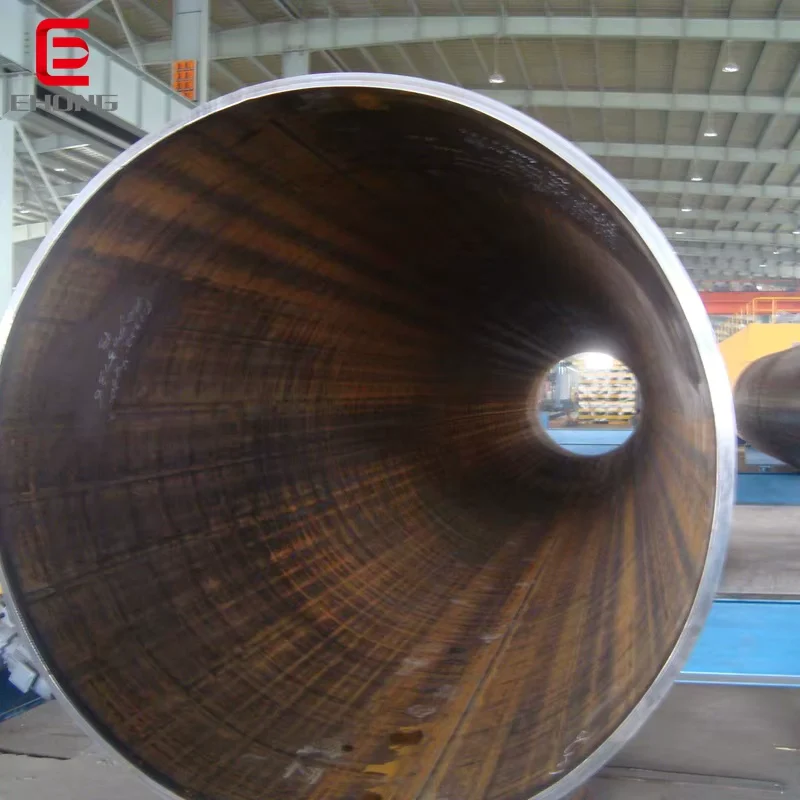
The LSAW process begins with steel plate or coil that is formed into a cylindrical shape and welded along a single longitudinal seam using submerged arc welding — a method where the arc is struck beneath a blanket of granular flux, shielding the molten weld pool from atmospheric contamination. This produces a weld deposit with low hydrogen content and minimal slag inclusion, critical for the integrity of high-pressure service. Steel grades such as Q235B and S235JR serve general structural and low-pressure fluid applications, while S275, S355, and API 5L Gr.B / Gr.C are specified where higher yield strength reduces the required wall thickness for a given design pressure. The Q-series (Chinese GB standard) and S-series (European EN standard) have direct equivalence mappings to ASTM A53 and A500 grades, but the mill test certificate must reference the exact standard called off on the purchase order — mixing designations on documentation causes rejection at third-party inspection. [NEED_CITE: steel grade equivalence mapping between EN 10219 and ASTM A500]
The Hidden Cost of Unverified Wall Thickness and Missing Heat Numbers
Procuring LSAW welded steel pipe without independent verification of wall thickness tolerance and heat-number traceability creates costs that never appear on the initial purchase invoice. Pipes with wall thickness below the specified minimum will fail hydrostatic testing at the project site, requiring either pipe replacement at multiples of the original cost or engineering re-assessment that delays commissioning. Missing or incomplete mill test certificates — particularly those not tied to individual heat numbers — trigger customs holds in markets with strict import documentation requirements, from Nigeria to the UAE to Brazil. [NEED_CITE: import documentation requirements for steel pipe with CE marking] The cost of a third-party SGS or BV pre-shipment inspection is a fraction of the cost of a rejected container at the destination port.
Why Global Buyers Source LSAW Pipe Through Our Jinan Mill
We operate three dedicated LSAW production lines in Jinan with monthly capacity exceeding 20,000 tons, meaning every order — from a single-ton trial to full-container bulk — is manufactured and inspected under our direct control rather than brokered through a trading desk. Our in-house metallurgical laboratory tests every heat for chemical composition and mechanical properties before the pipe leaves the mill, and the original mill test certificate travels with each shipment. For buyers who require independent verification, we accommodate SGS and BV third-party inspections at our facility before container loading. We maintain ready stock across 2,800+ specifications in standard sizes, and for non-standard OD, wall thickness, or length requirements, our production team provides custom quotations with typical lead times rather than catalog-only limitations. Every export shipment includes optimized container loading plans prepared by our dedicated export team, with complete documentation for customs clearance at the destination port.
Documentation & Compliance
- Mill test certificate documenting Q235B / API 5L Gr.B chemical composition and mechanical properties per the specified standard, with heat number traceability for every pipe in the shipment
- CE certificate under EN10210 / EN10219 for structural hollow sections shipped to European Union and EFTA markets
- ISO 9001:2015 quality management system certificate covering the full production and inspection process
- SGS or BV third-party inspection report available on request, covering dimensional checks, visual weld examination, and witness testing
- Material traceability report linking each pipe to its parent heat number, plate batch, and production date
- Full customs document package including commercial invoice, packing list, bill of lading, and certificate of origin
Packaging, Loading & Delivery
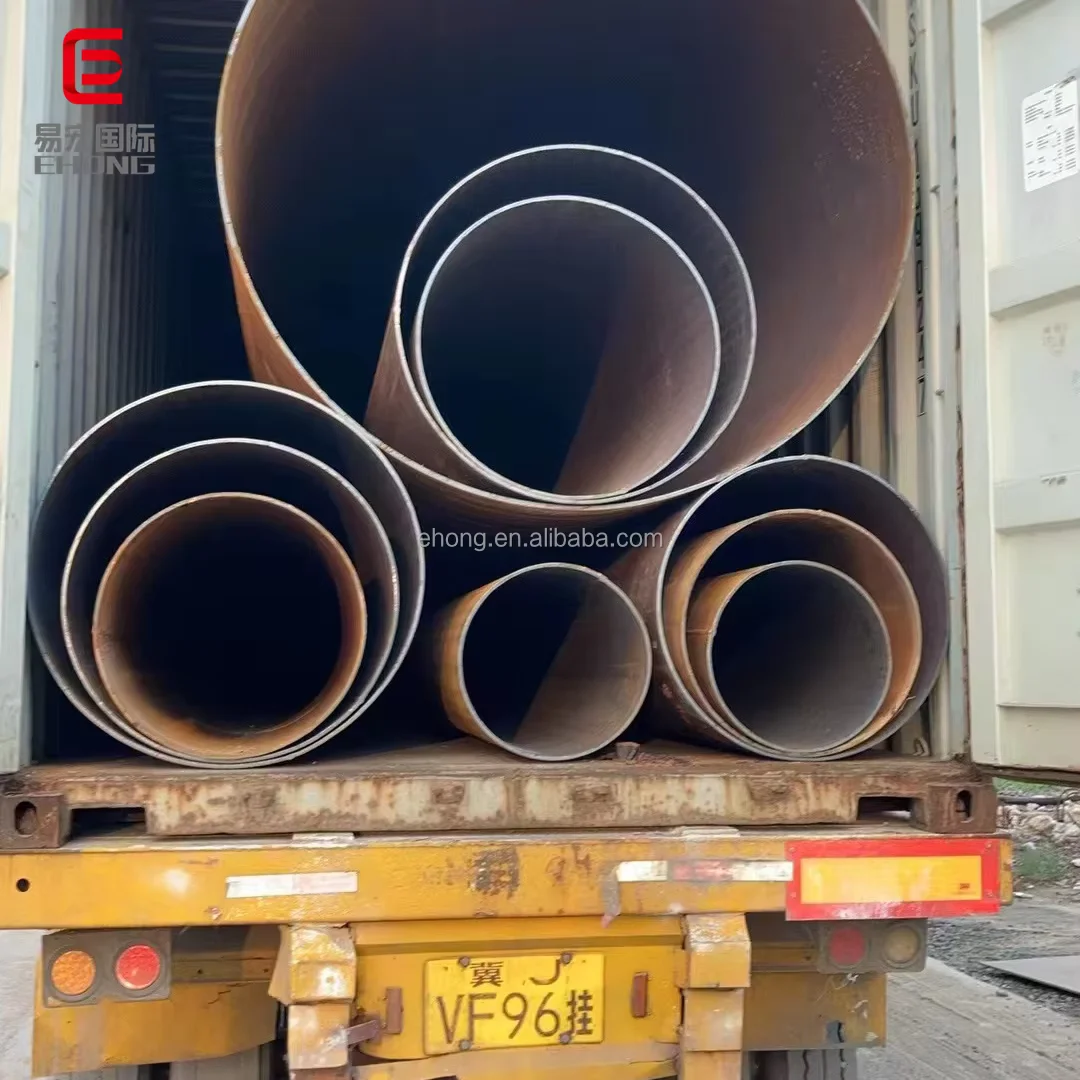
- LSAW pipes with OD ≥273 mm shipped as loose pieces with protective end caps on bevel ends; smaller OD pipes bundled with steel strips and nested for container space efficiency
- Black paint or oil-coated surfaces protected by anti-rust wrapping and edge protectors to preserve finish integrity during ocean transit
- 3PE and FBE coated pipes handled with nylon slings and padded separators to prevent coating damage during loading and transport
- Custom cut lengths between 3–12 m accommodated, with length tolerance documented on the packing list and pipe markings
- Heat number, steel grade, OD, and wall thickness stenciled on each pipe at intervals per standard export practice
- FOB, CIF, and DDP shipping terms available with container loading optimization for 20 ft and 40 ft open-top or flat-rack containers depending on pipe diameter
Getting a Firm Quotation on Your LSAW Pipe Requirement
Submit your specification sheet — including OD, wall thickness, length, steel grade, surface treatment, quantity, and destination port — and our technical team returns a detailed quotation within 12 hours, complete with mill test certificate format confirmation and third-party inspection arrangement if required. For non-standard dimensions or project-specific coating requirements, we provide a custom production assessment rather than a catalog refusal.
Request Your LSAW Pipe Quotation with Mill Test Certificate
Send your specification and quantity to our technical team for a factory-direct quotation with full documentation support.
Mobile / WhatsApp / WeChat: +86 188 5315 7756 | Email: admin@sdxinjiyuan.com
Frequently Asked Questions
Q: What is the difference between LSAW and ERW welded steel pipe for high-pressure applications?
A: LSAW welded steel pipe uses a submerged arc welding process that produces a full-penetration weld seam with superior toughness, making it the preferred choice for large-diameter (406–1524 mm OD) and thick-wall (8–60 mm) applications such as oil and gas transmission pipelines. ERW pipe is typically limited to smaller diameters and lower pressure ratings.
Q: Which steel grade should I specify for a buried water transmission pipeline?
A: For municipal water mains operating at moderate pressure, Q235B or S235JR is commonly specified. For higher-pressure transmission or larger diameters where wall thickness optimization matters, S275 or S355 provides higher yield strength. The final selection depends on design pressure, burial depth, and the applicable engineering code.
Q: Can you provide third-party inspection before shipment?
A: Yes. We accommodate SGS and BV third-party inspections at our Jinan facility on request. The inspection covers dimensional verification, visual weld examination, and witness testing, with the report issued before container loading.
Q: What surface treatment is recommended for a pipeline in a corrosive soil environment?
A: For buried pipelines in corrosive environments, 3PE (three-layer polyethylene) coating provides the highest level of external corrosion protection. FBE (fusion-bonded epoxy) is suitable for high-temperature service. Epoxy painting and black paint serve less aggressive conditions. The choice depends on soil resistivity data and design life.
Q: What is the minimum order quantity for LSAW welded steel pipe?
A: The MOQ is 1 Ton, with trial orders supported via LCL shipment for buyers testing our product quality before committing to bulk procurement. Standard sizes are available from ready stock for faster delivery.